PROJECT EVIDENCE
Engineering Case Studies
Compare project scale, feed or process stream, and the membrane sections actually used across tubular membrane engineering, industrial wastewater reuse and ZLD, and process-fluid separation.
Showing 25–36 of 72
All case studies
Industrial Wastewater Reuse & ZLD
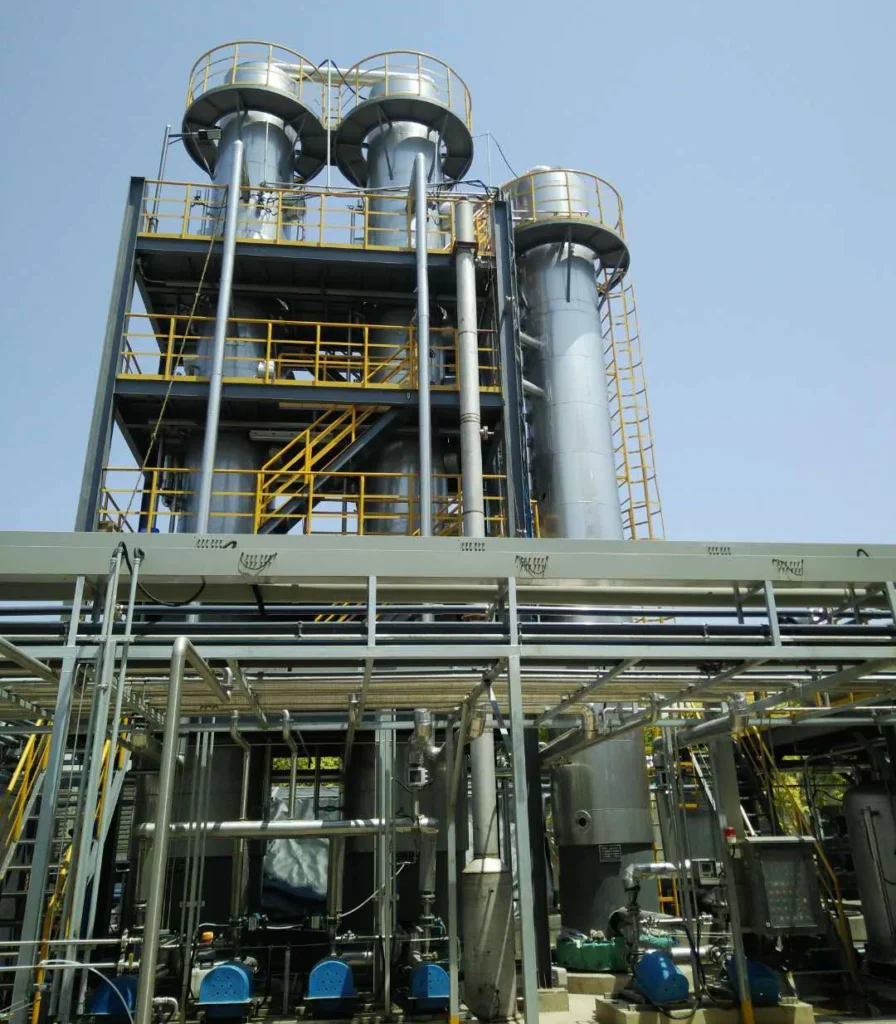
400 m³/d Landfill Leachate Ammonia Stripping Validation
Reduce front-end ammonia loading and define gas, liquid, absorption, and downstream biological interfaces.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →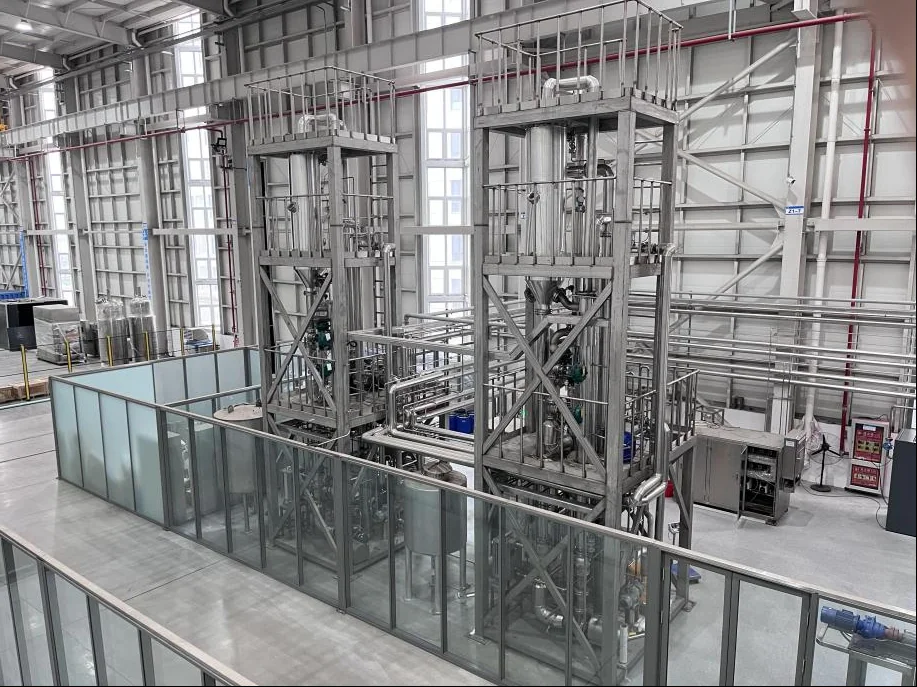
Industrial Wastewater Reuse & ZLD
500 L/h Lithium-Extraction Membrane Separation and Concentration Pilot
This 500 L/h pilot platform evaluates salt-lake brine and lithium-bearing ore-leach liquor. PEK tubular membranes, resin adsorption, nanofiltration and reverse osmosis are combined to validate clarification, selective separation and concentration.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →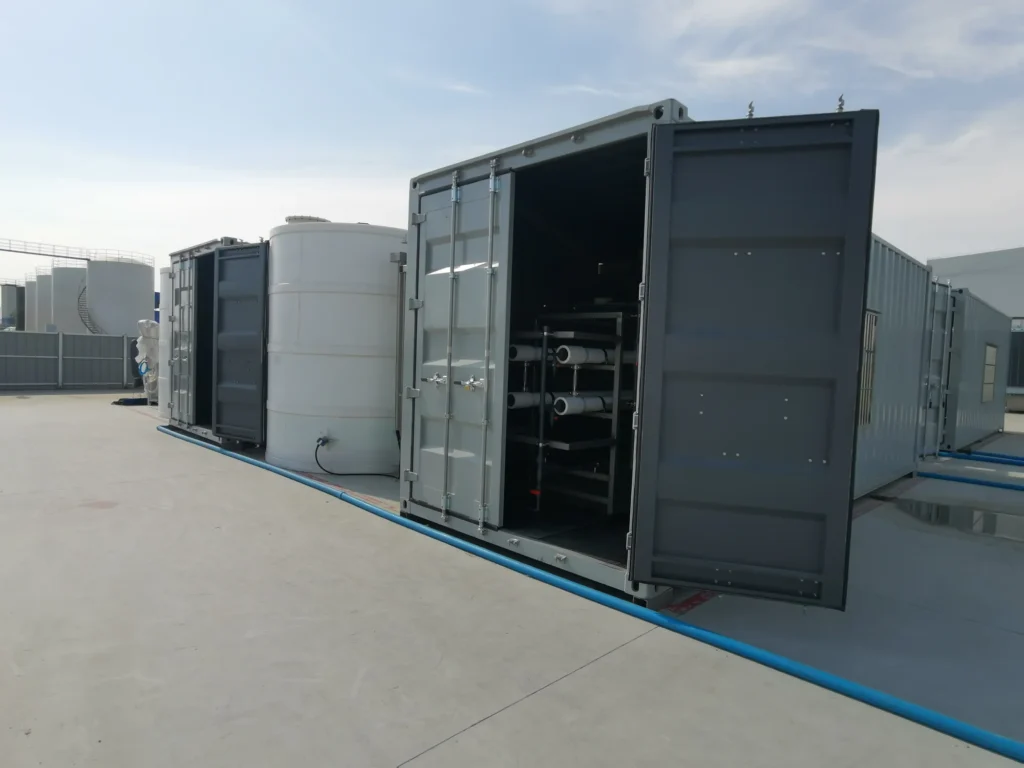
Industrial Wastewater Reuse & ZLD
200 kg/h Industrial Waste-Salt Resource-Recovery Pilot
This pilot processes industrial waste salt and its dissolution liquor at a capacity of 200 kg/h of solid waste salt. Dissolution, softening, tubular solid-liquid separation, NF salt separation, RO concentration and subsequent crystallization are combined to validate the resource-recovery route.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →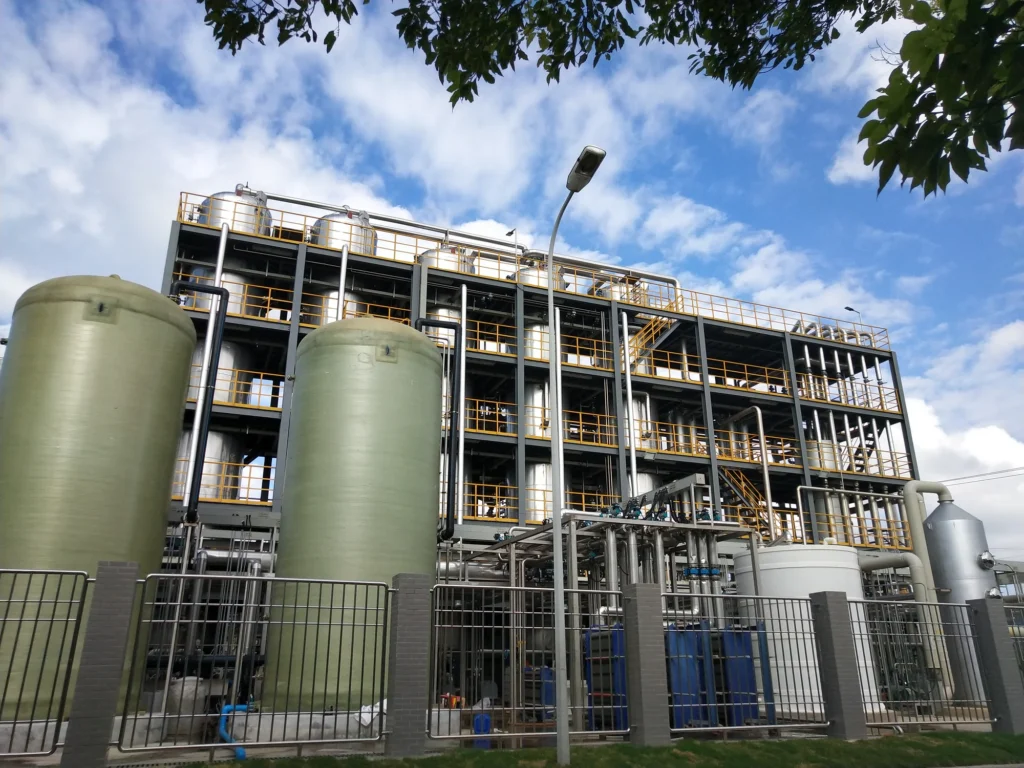
Industrial Wastewater Reuse & ZLD
2,000 m³/d Aged Landfill Leachate Ammonia Stripping and Recovery Project
This 2,000 m³/d project treats aged landfill leachate through filtration, preheating, ammonia stripping, carbonation absorption and centrifugation. The route reduces the incoming ammonia load and links to ammonium-bicarbonate recovery.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →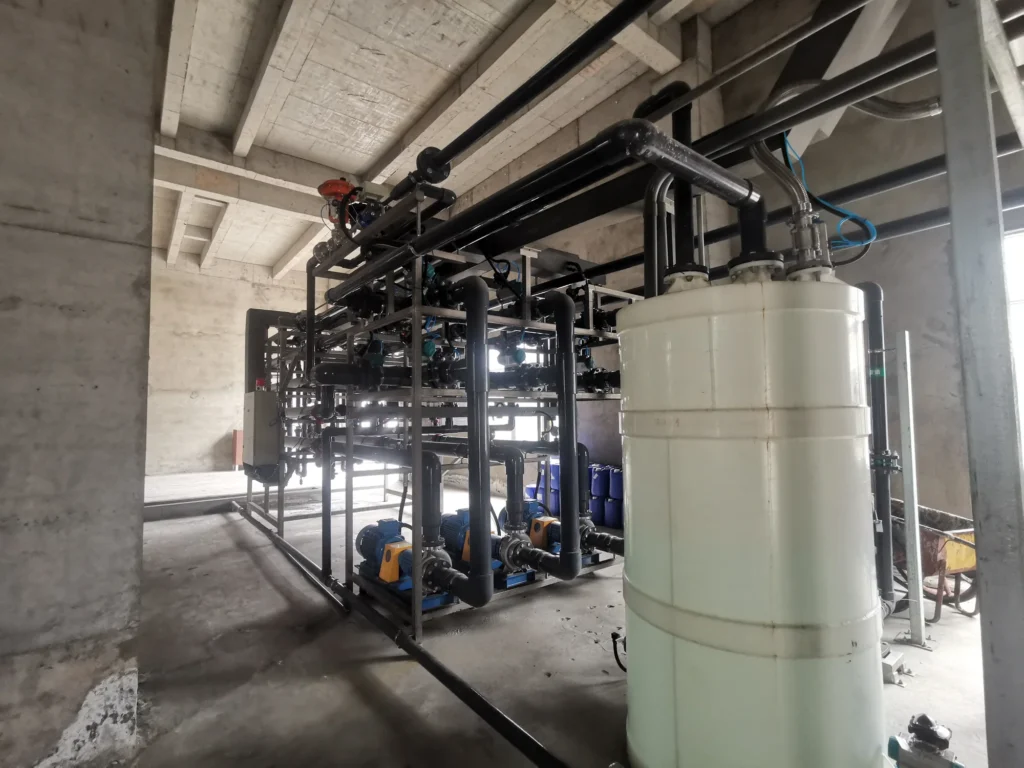
Industrial Wastewater Reuse & ZLD
40 m³/h Vanadium-Mine Wastewater Softening and Membrane Treatment Project
This 40 m³/h project treats wastewater from vanadium-mine operations. Chemical softening and PEK tubular solid-liquid separation are followed by nanofiltration and reverse-osmosis concentration.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →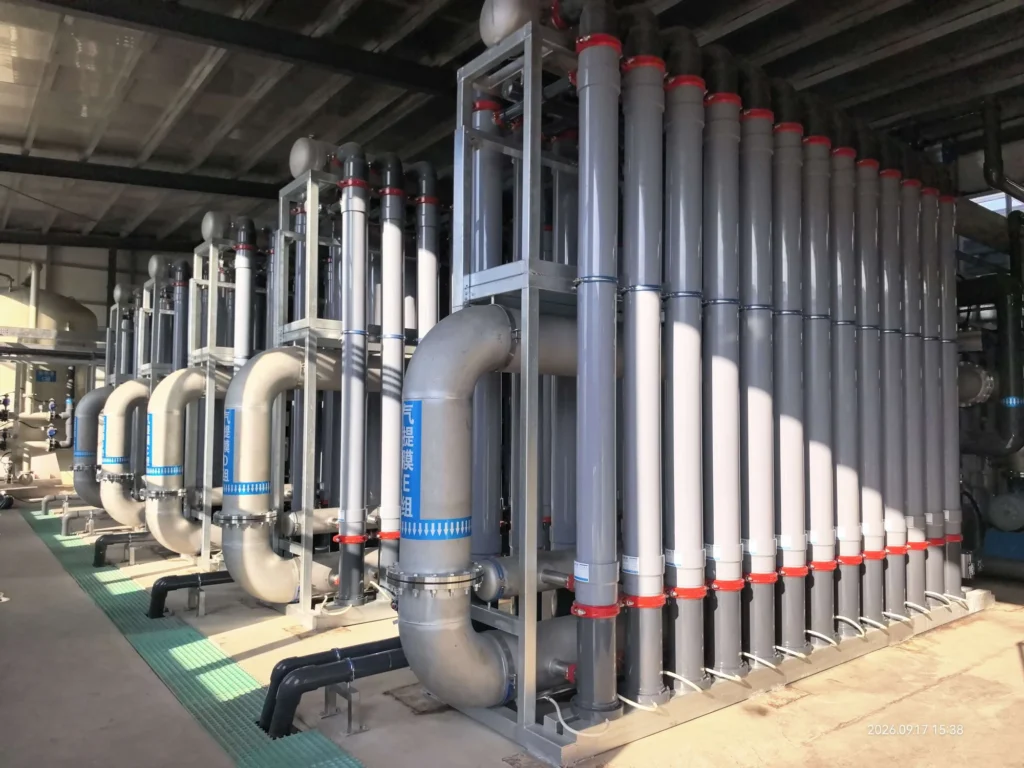
Industrial Wastewater Reuse & ZLD
5,000 m³/d Corn-Processing Wastewater Air-Lift MBR and Reuse Project
This 5,000 m³/d project treats corn-processing wastewater using biological treatment, PEK Air-Lift MBR, reverse osmosis and activated-carbon adsorption for deep treatment and water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →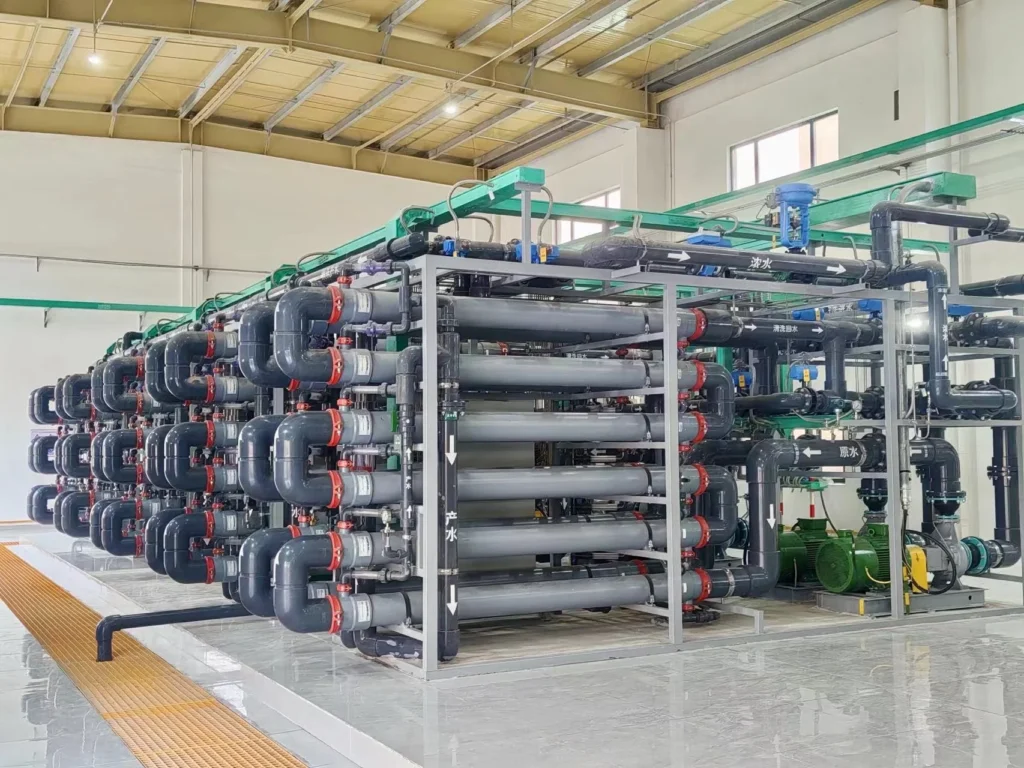
Industrial Wastewater Reuse & ZLD
400 m³/h Photovoltaic Plant Cooling-Blowdown Reuse Project
This project treats 400 m³/h of cooling blowdown from a photovoltaic plant. Softening, PEK tubular membrane clarification and HRCC reverse-osmosis concentration are combined for blowdown reduction and water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →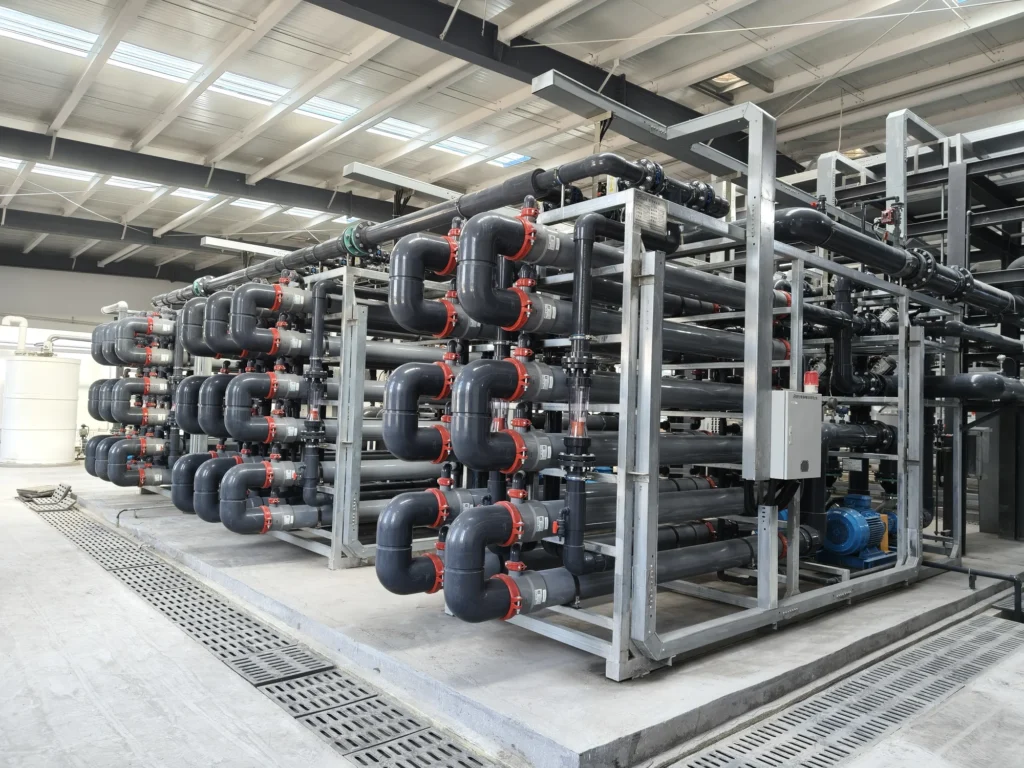
Industrial Wastewater Reuse & ZLD
4,500 m³/d High-Salinity Mine-Water Reuse Project
This 4,500 m³/d project treats high-salinity, high-hardness mine water. Dual-alkali softening, alkali-resistant tubular ultrafiltration and reverse-osmosis concentration are combined for reuse in mine production and auxiliary water systems.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →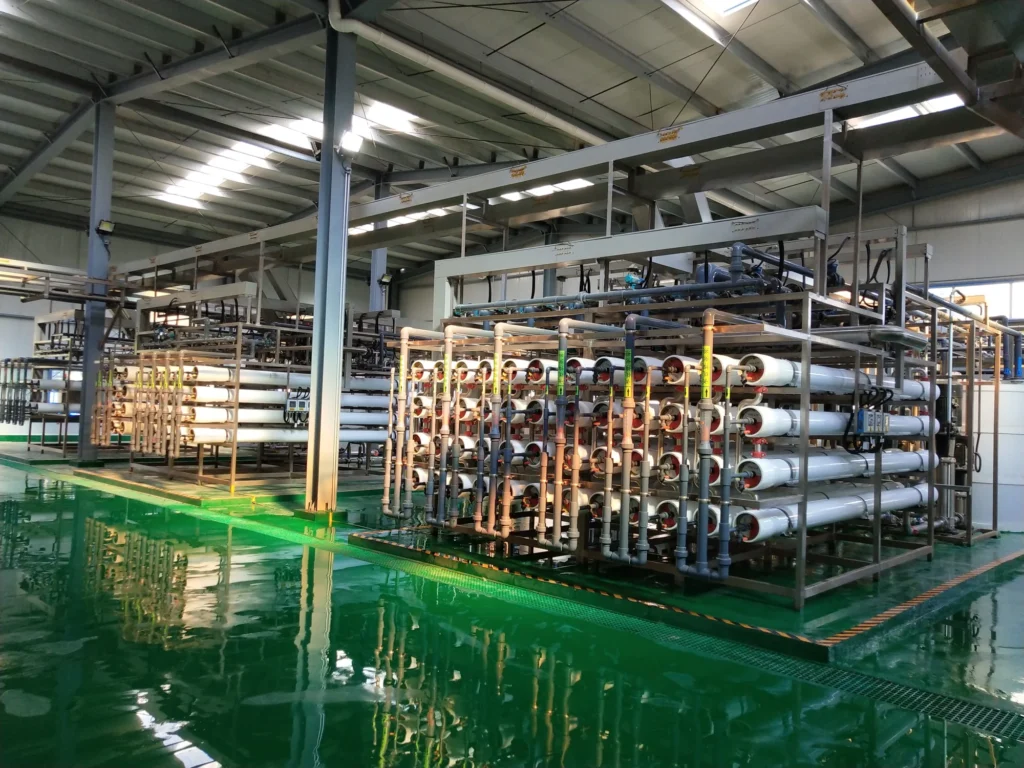
Industrial Wastewater Reuse & ZLD
3,200 m³/d Leachate and 640 m³/d Concentrate NF Treatment Project
This project has separate duties of 3,200 m³/d for landfill leachate and 640 m³/d for concentrate. Nanofiltration splitting and multistage concentrate treatment organize the permeate and concentrate streams for subsequent handling.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →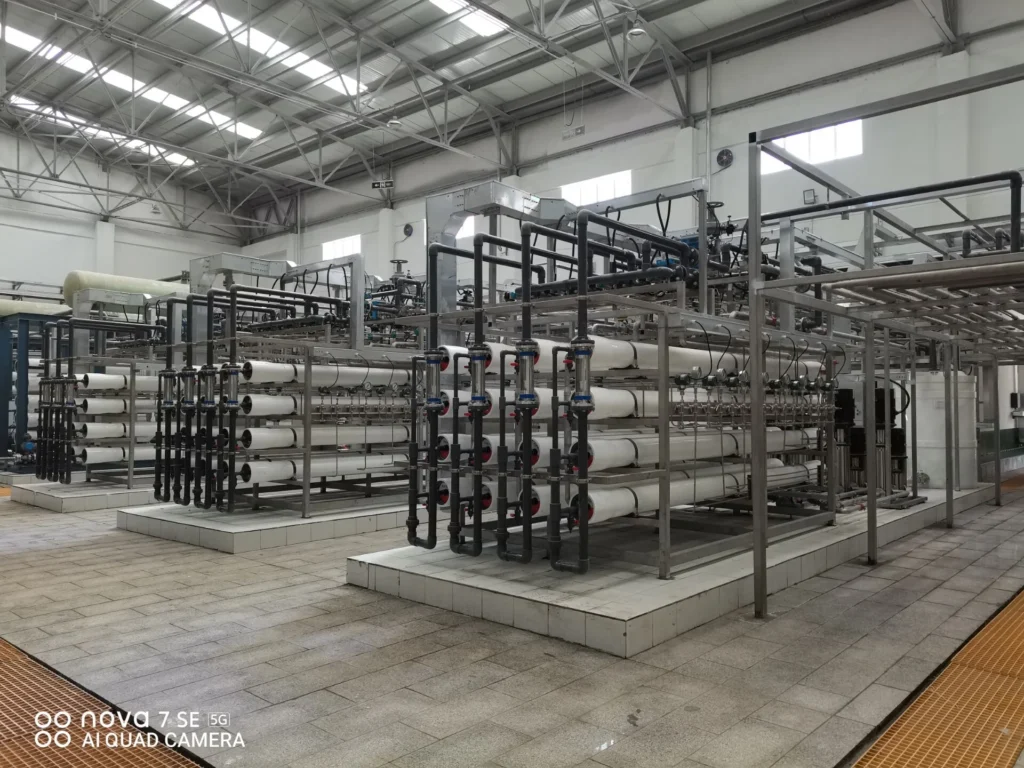
Industrial Wastewater Reuse & ZLD
25 m³/h Coal-Chemical Brine Salt-Separation Phase II Project
This phase II project treats 25 m³/h of coal-chemical RO brine. Ultrafiltration, nanofiltration salt separation, evaporation and crystallization are combined to process the resulting salt fractions.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →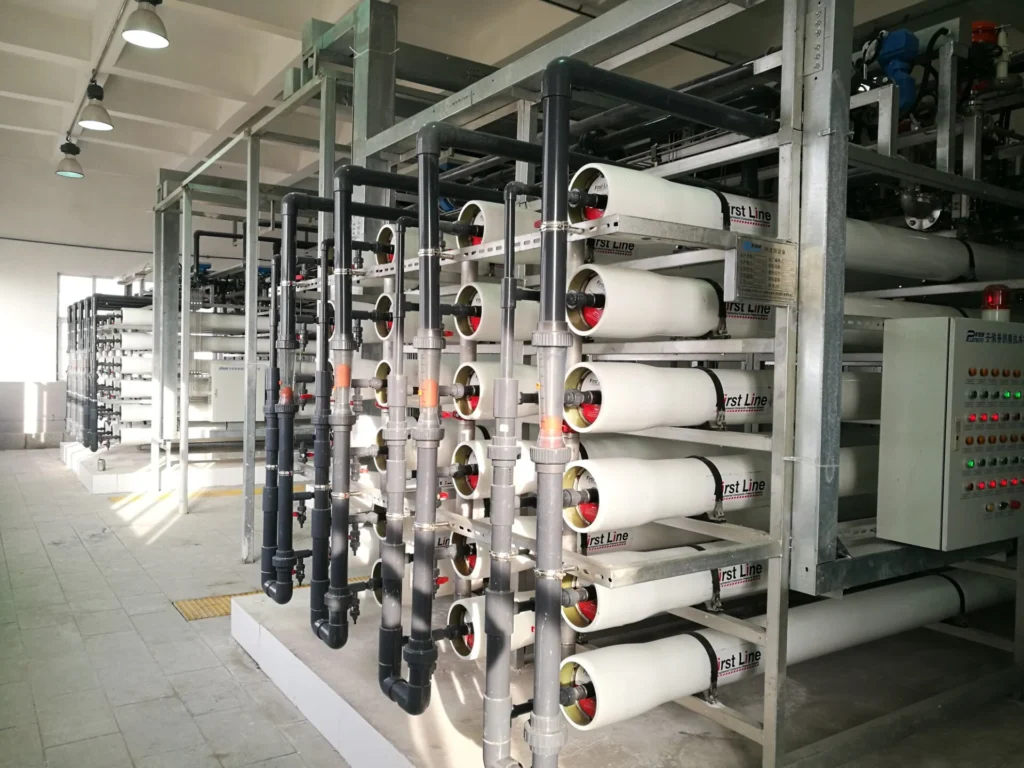
Industrial Wastewater Reuse & ZLD
60 m³/h RO Brine and 4 m³/h Mother-Liquor Salt-Separation Project
This coal-chemical project treats 60 m³/h of RO brine and 4 m³/h of crystallization mother liquor. The process combines ultrafiltration, two-stage nanofiltration, evaporation and crystallization, with a dedicated mother-liquor recovery duty.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →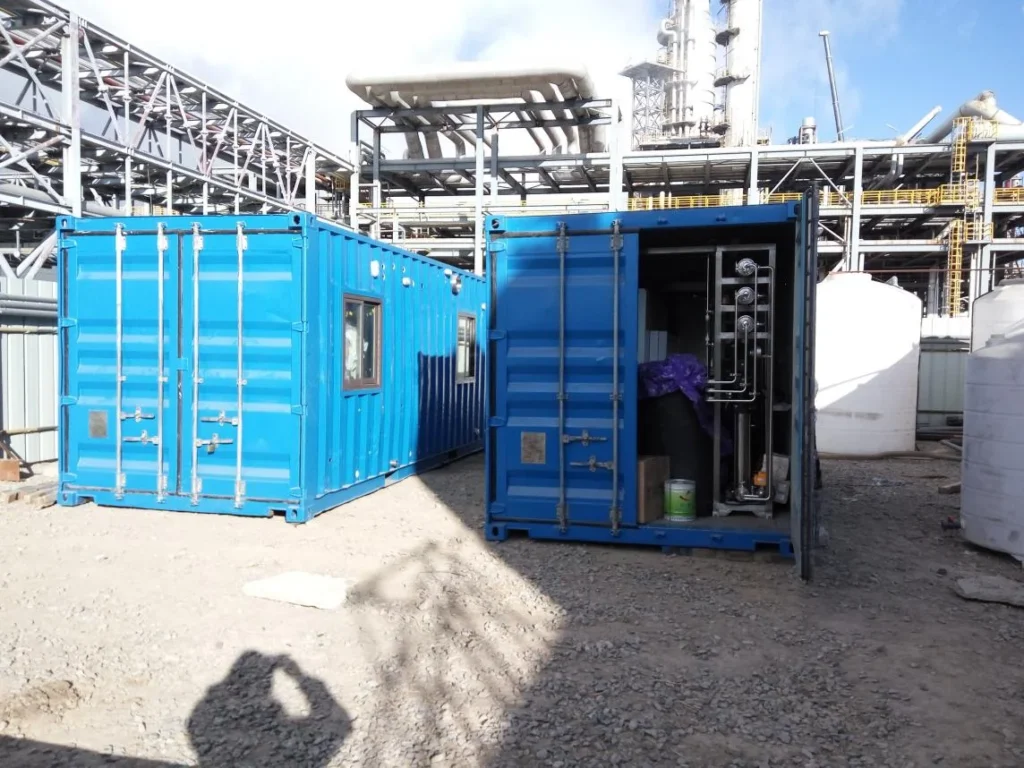
Industrial Wastewater Reuse & ZLD
24 m³/d RO Brine Reuse and Salt-Separation Pilot
This 24 m³/d pilot treats RO brine from coal-chemical production. Ultrafiltration and two-stage nanofiltration are combined to evaluate water reuse and selective salt treatment.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →PROJECT CONTEXT