PROJECT EVIDENCE
Engineering Case Studies
Compare project scale, feed or process stream, and the membrane sections actually used across tubular membrane engineering, industrial wastewater reuse and ZLD, and process-fluid separation.
Showing 1–12 of 23
02 · INDUSTRIAL WATER
Industrial Wastewater Reuse & ZLD
References documenting reuse, brine, concentration, and leachate membrane sections with explicit project boundaries.
Industrial Wastewater Reuse & ZLD
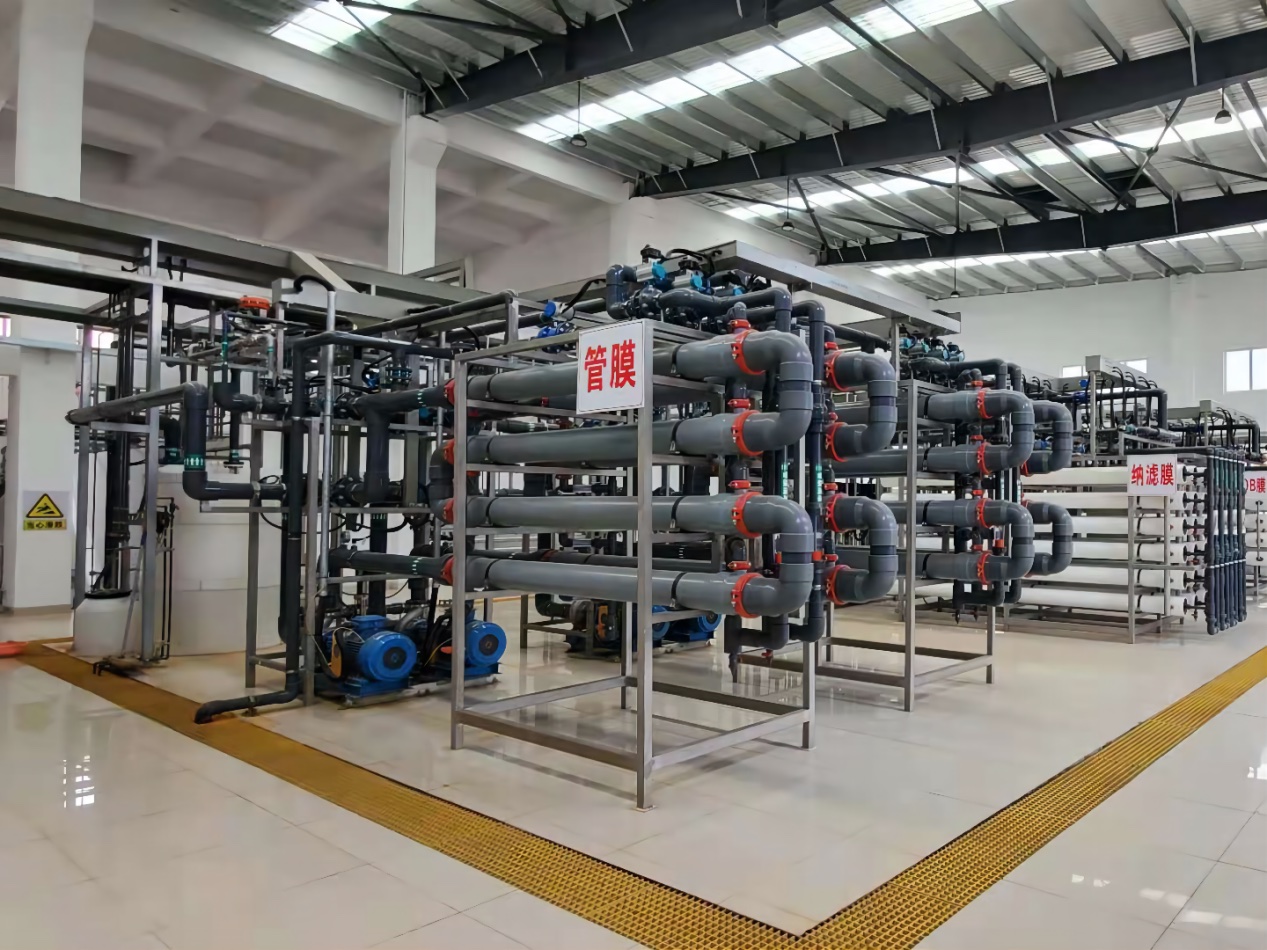
1,350 m³/d Pickling Wastewater Metals & Hardness Removal
This 1,350 m³/d steel pickling wastewater project combines iron-removal and softening pretreatment, tubular membrane separation, nanofiltration salt separation, reverse osmosis concentration, and evaporation and crystallization for water reuse and salt resource recovery.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →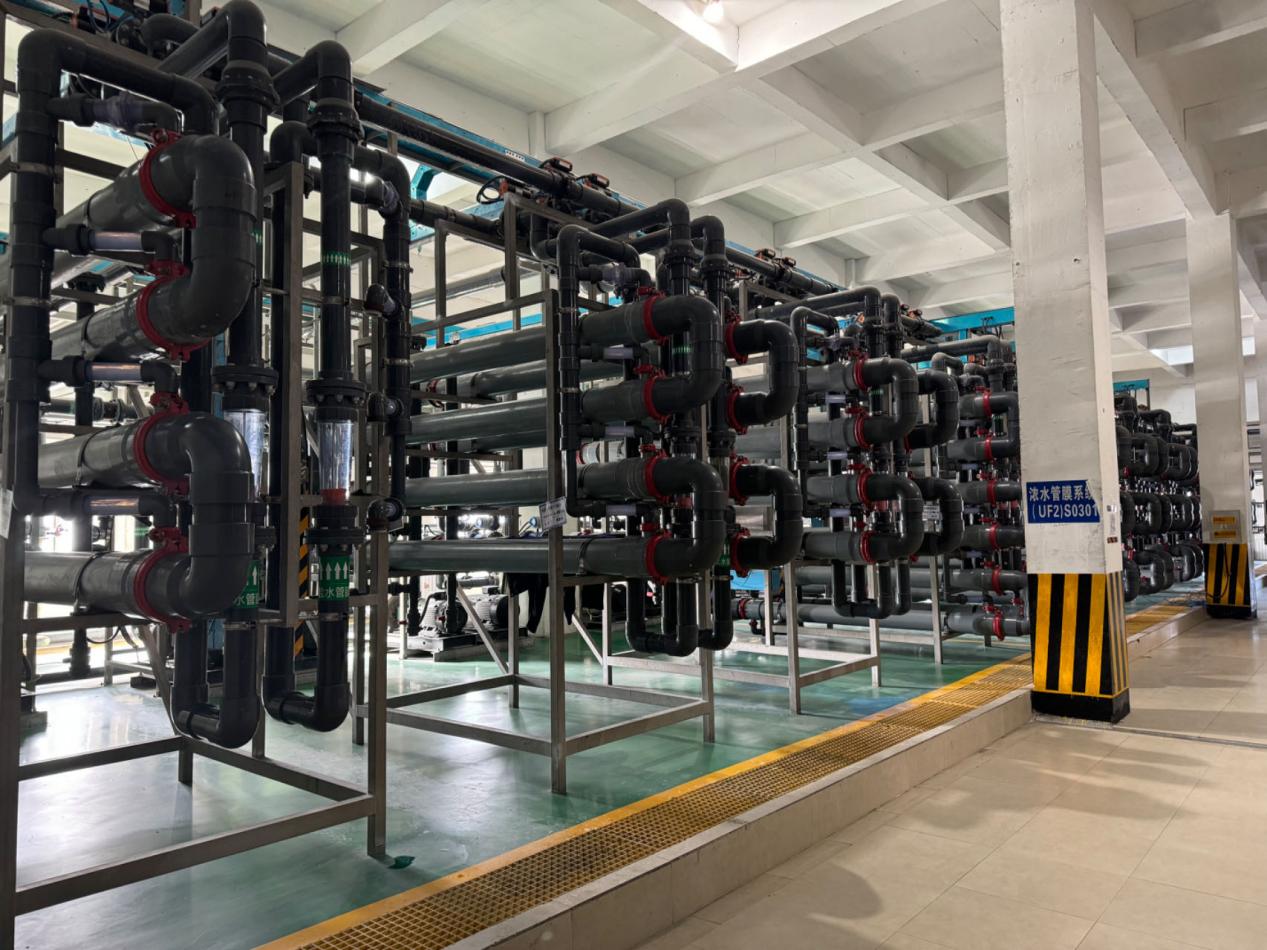
Industrial Wastewater Reuse & ZLD
235 + 106 m³/h Reclaimed Water & RO Brine Treatment
Manage separate reclaimed-water and RO-brine duties before project-defined reuse, fractionation, concentration, or terminal sections.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →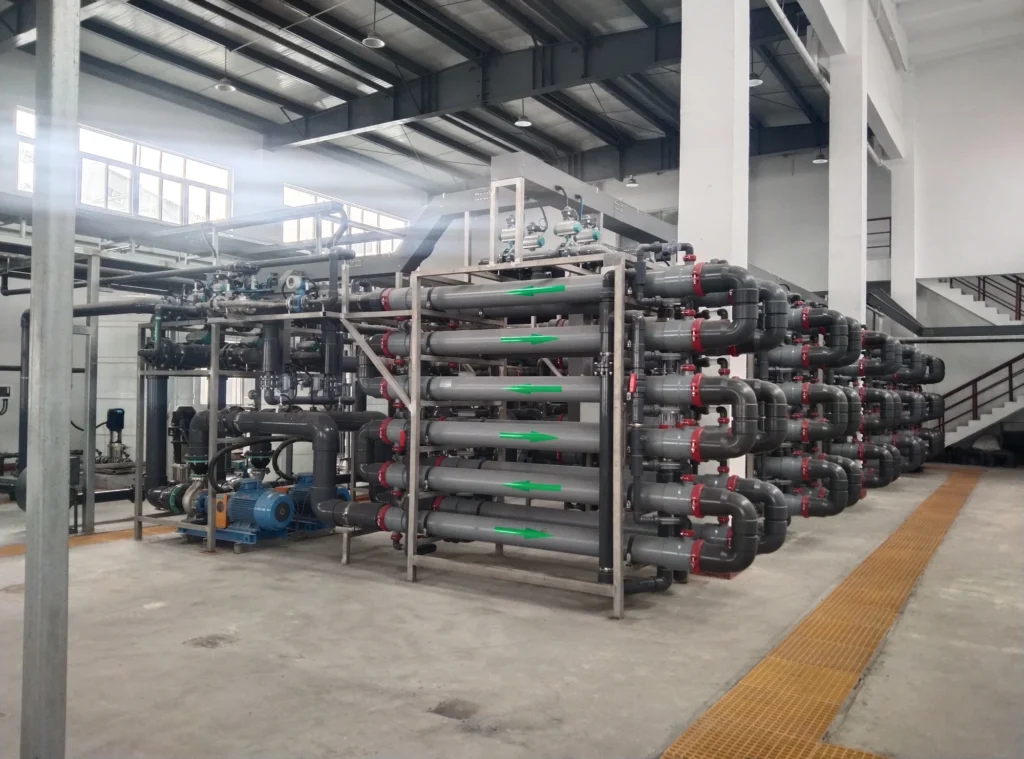
Industrial Wastewater Reuse & ZLD
150 m³/h Mine Water Reuse & ZLD
Define reuse and concentrate routes from actual mine-water chemistry and project endpoints.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →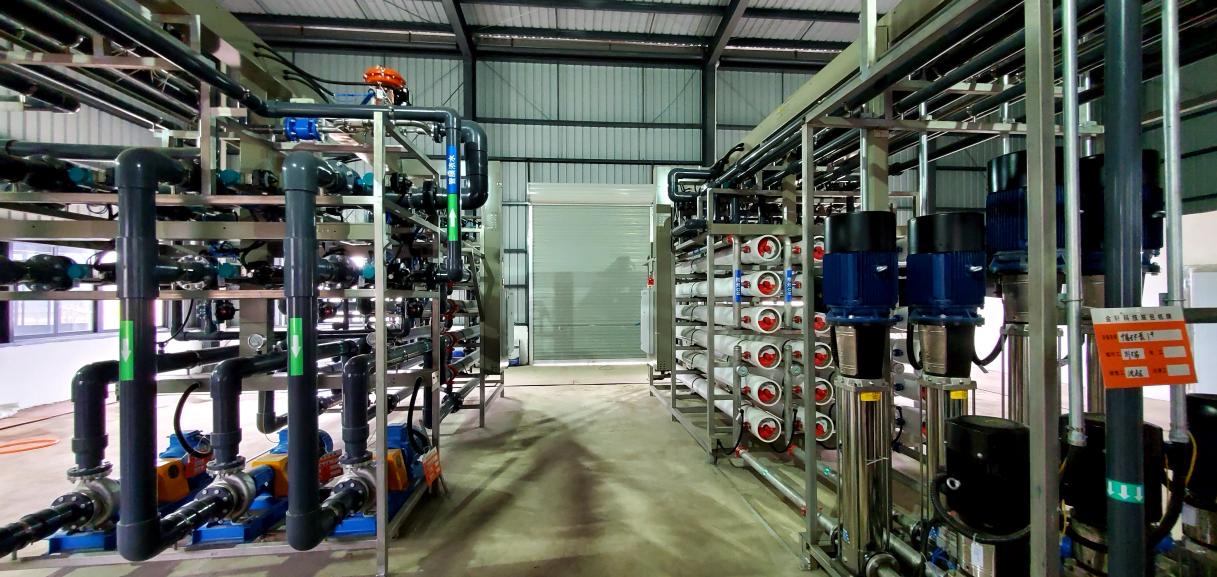
Industrial Wastewater Reuse & ZLD
52 m³/h Cooling-Tower Blowdown Reuse
Control scaling and suspended solids before project-specific desalination, reuse, and concentrate management.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →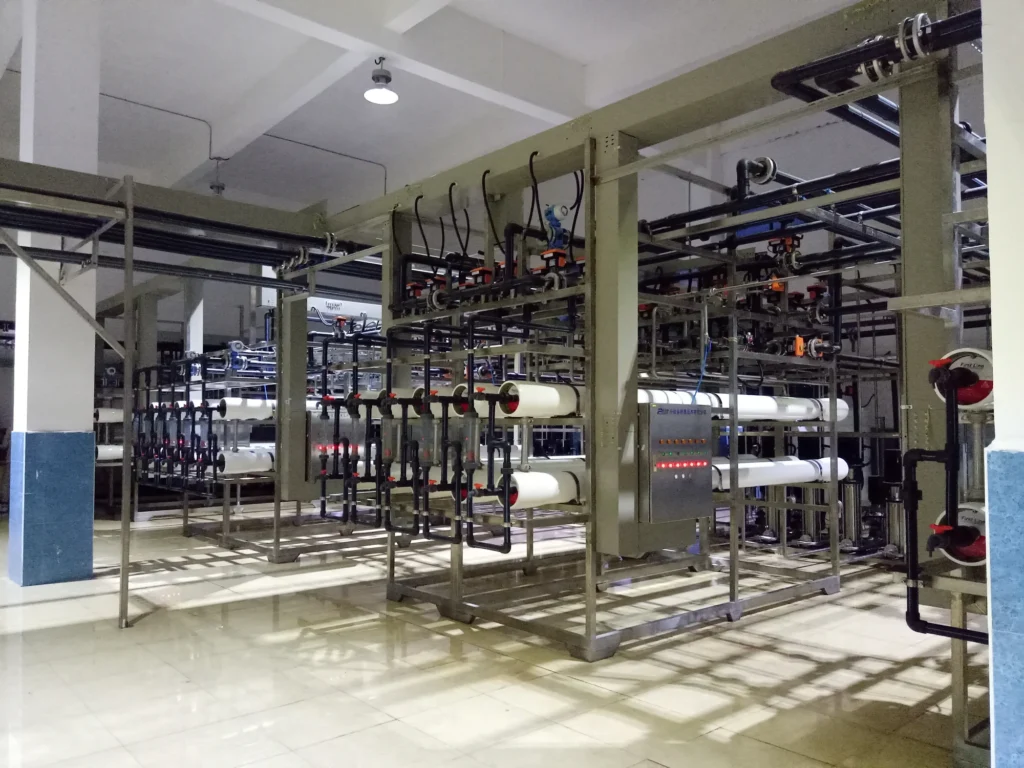
Industrial Wastewater Reuse & ZLD
425 + 300 m³/d Landfill Leachate Multistage NF
Organize selective organic/inorganic fractionation while defining every permeate and concentrate endpoint separately.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →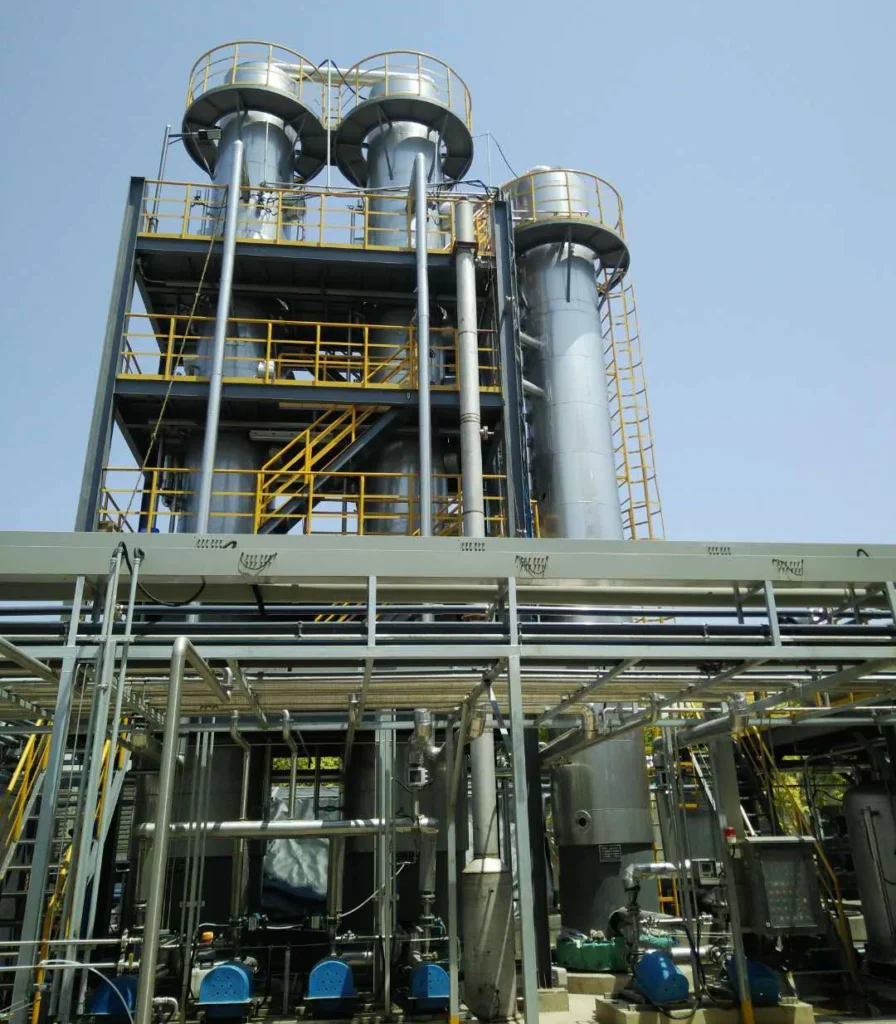
Industrial Wastewater Reuse & ZLD
400 m³/d Landfill Leachate Ammonia Stripping Validation
Reduce front-end ammonia loading and define gas, liquid, absorption, and downstream biological interfaces.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →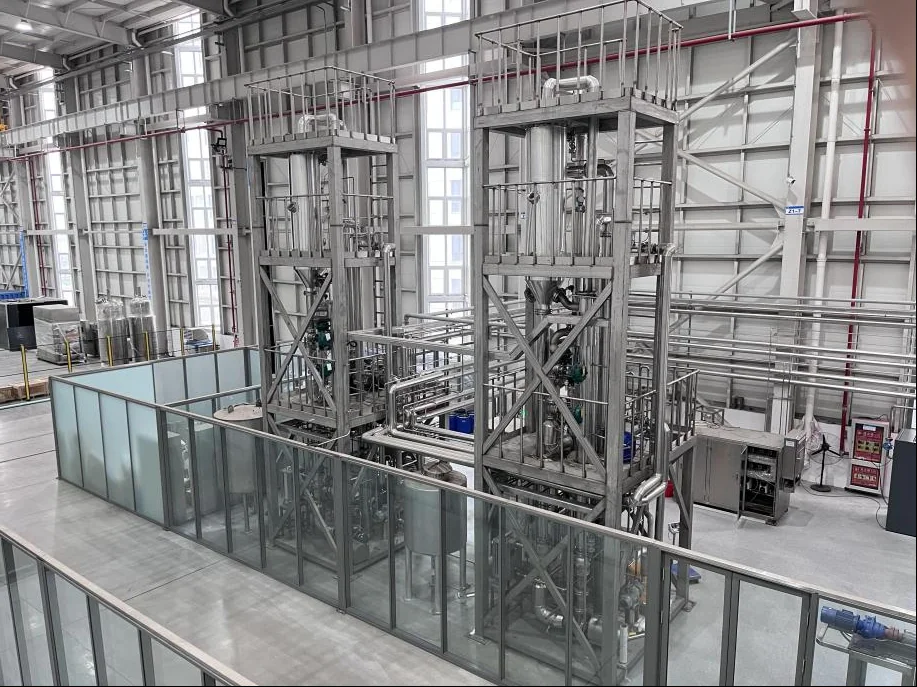
Industrial Wastewater Reuse & ZLD
500 L/h Lithium-Extraction Membrane Separation and Concentration Pilot
This 500 L/h pilot platform evaluates salt-lake brine and lithium-bearing ore-leach liquor. PEK tubular membranes, resin adsorption, nanofiltration and reverse osmosis are combined to validate clarification, selective separation and concentration.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →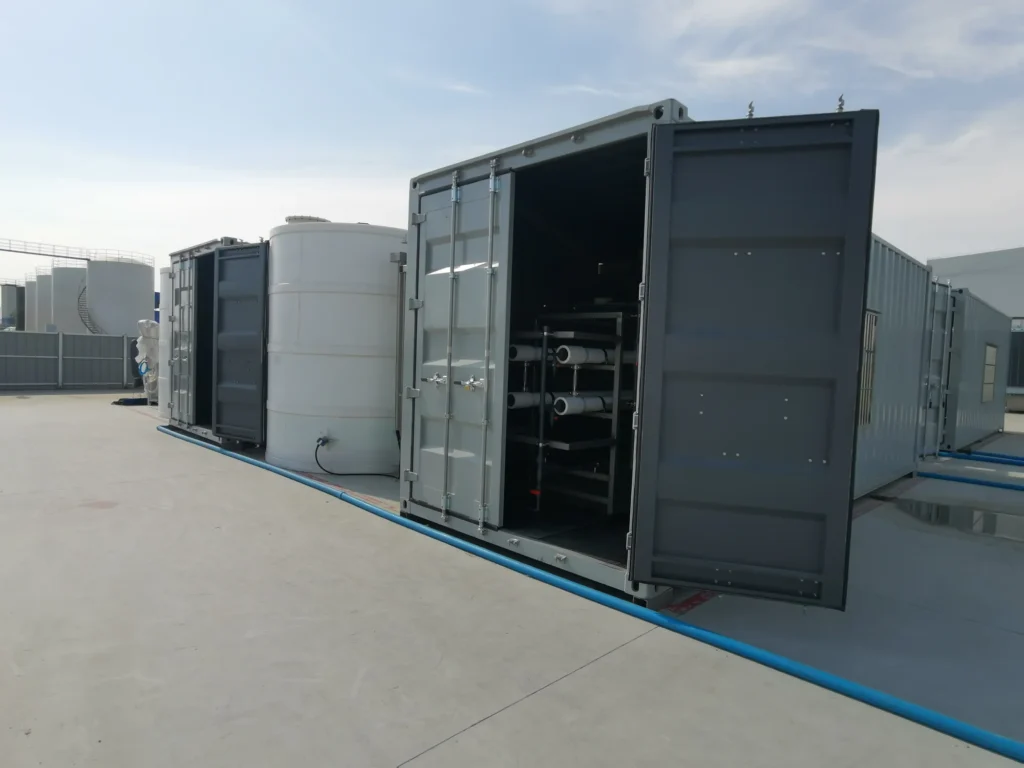
Industrial Wastewater Reuse & ZLD
200 kg/h Industrial Waste-Salt Resource-Recovery Pilot
This pilot processes industrial waste salt and its dissolution liquor at a capacity of 200 kg/h of solid waste salt. Dissolution, softening, tubular solid-liquid separation, NF salt separation, RO concentration and subsequent crystallization are combined to validate the resource-recovery route.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →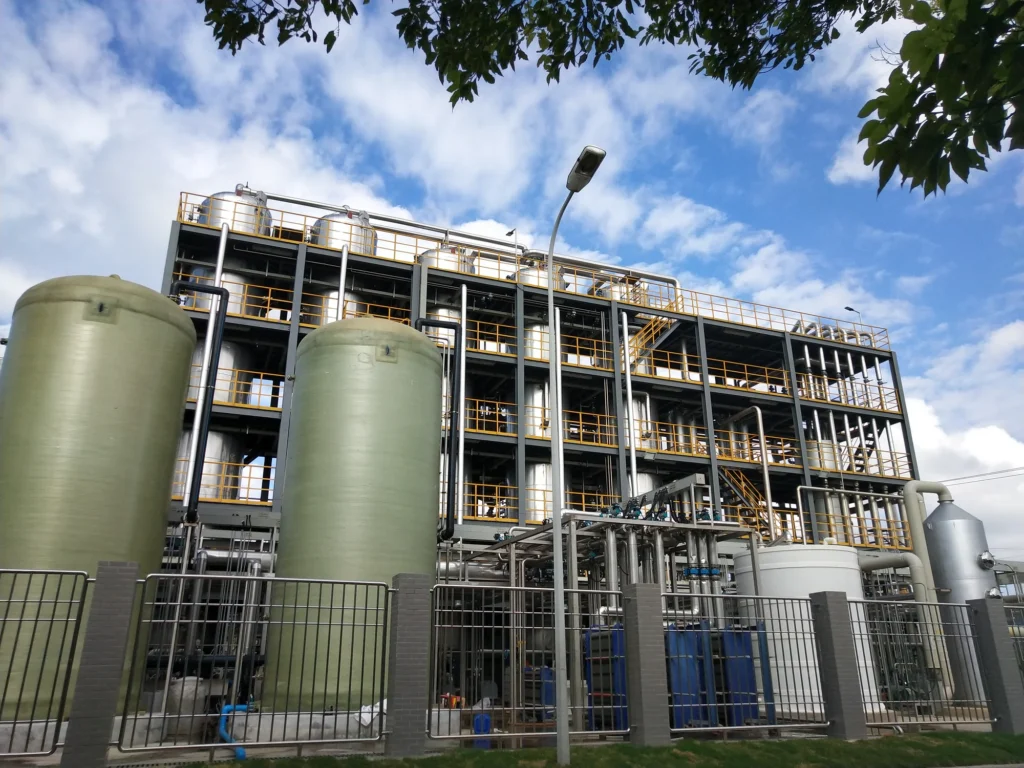
Industrial Wastewater Reuse & ZLD
2,000 m³/d Aged Landfill Leachate Ammonia Stripping and Recovery Project
This 2,000 m³/d project treats aged landfill leachate through filtration, preheating, ammonia stripping, carbonation absorption and centrifugation. The route reduces the incoming ammonia load and links to ammonium-bicarbonate recovery.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →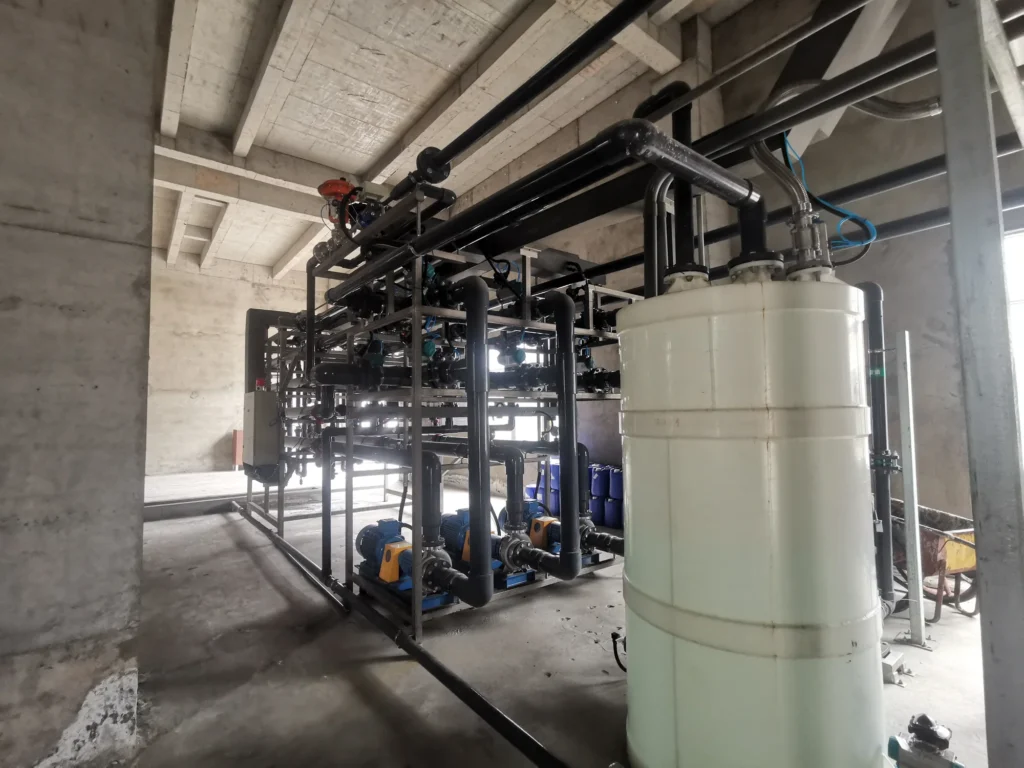
Industrial Wastewater Reuse & ZLD
40 m³/h Vanadium-Mine Wastewater Softening and Membrane Treatment Project
This 40 m³/h project treats wastewater from vanadium-mine operations. Chemical softening and PEK tubular solid-liquid separation are followed by nanofiltration and reverse-osmosis concentration.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →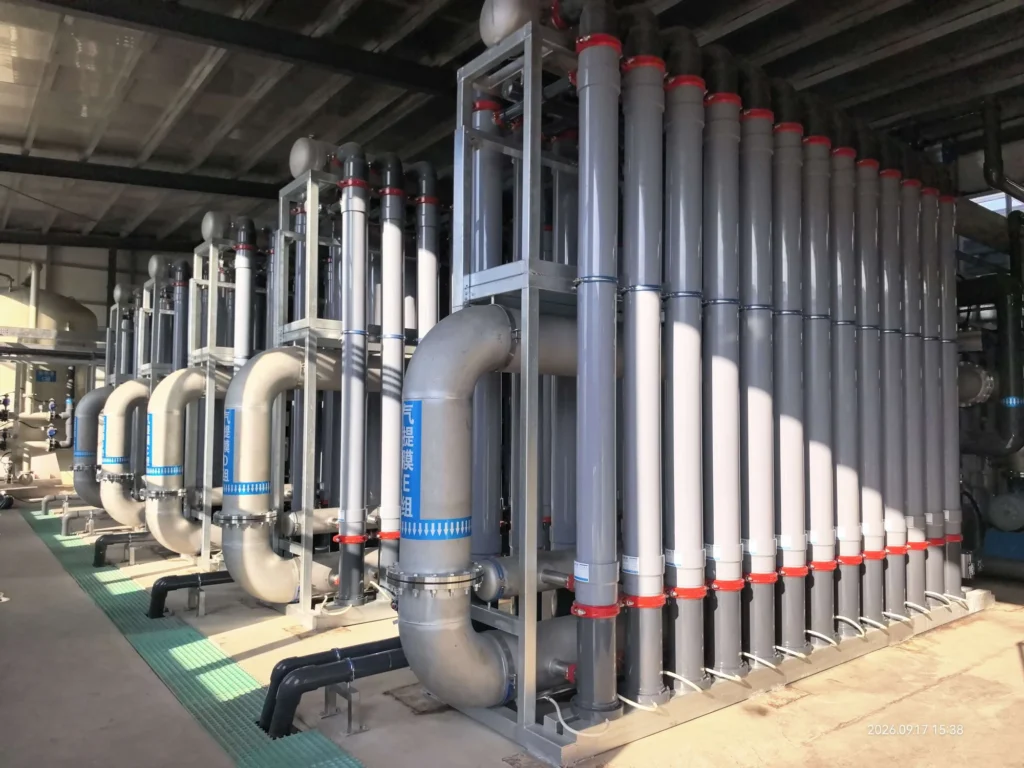
Industrial Wastewater Reuse & ZLD
5,000 m³/d Corn-Processing Wastewater Air-Lift MBR and Reuse Project
This 5,000 m³/d project treats corn-processing wastewater using biological treatment, PEK Air-Lift MBR, reverse osmosis and activated-carbon adsorption for deep treatment and water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →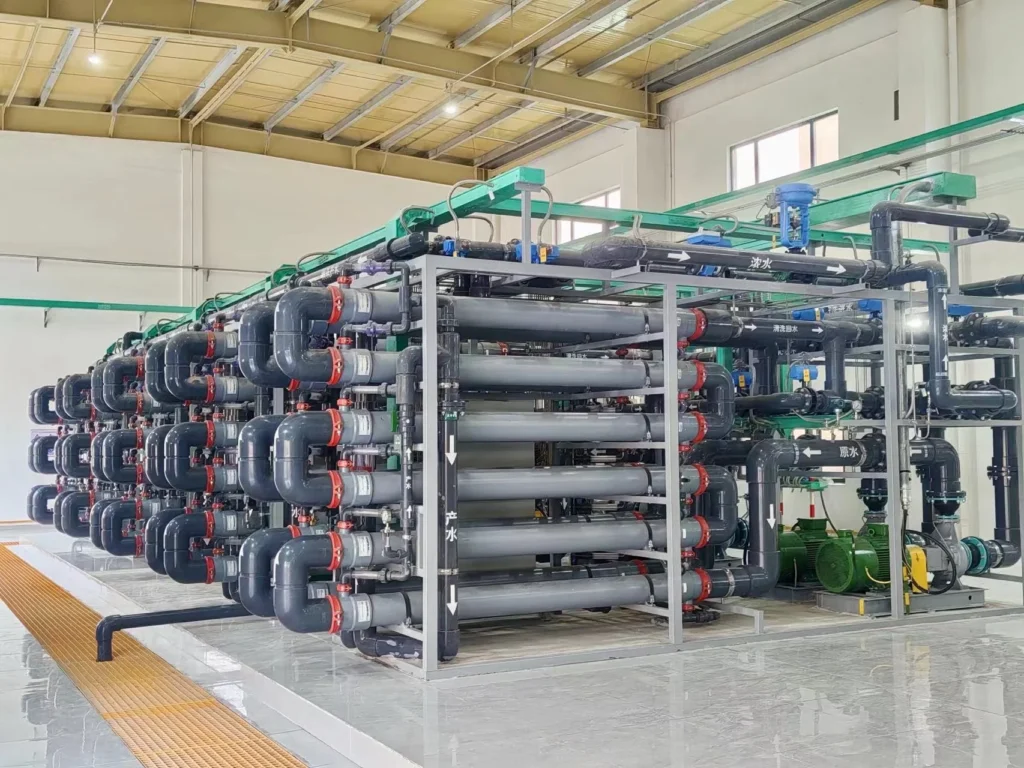
Industrial Wastewater Reuse & ZLD
400 m³/h Photovoltaic Plant Cooling-Blowdown Reuse Project
This project treats 400 m³/h of cooling blowdown from a photovoltaic plant. Softening, PEK tubular membrane clarification and HRCC reverse-osmosis concentration are combined for blowdown reduction and water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →PROJECT CONTEXT