PROJECT EVIDENCE
Engineering Case Studies
Compare project scale, feed or process stream, and the membrane sections actually used across tubular membrane engineering, industrial wastewater reuse and ZLD, and process-fluid separation.
Showing 37–48 of 72
All case studies
Industrial Wastewater Reuse & ZLD
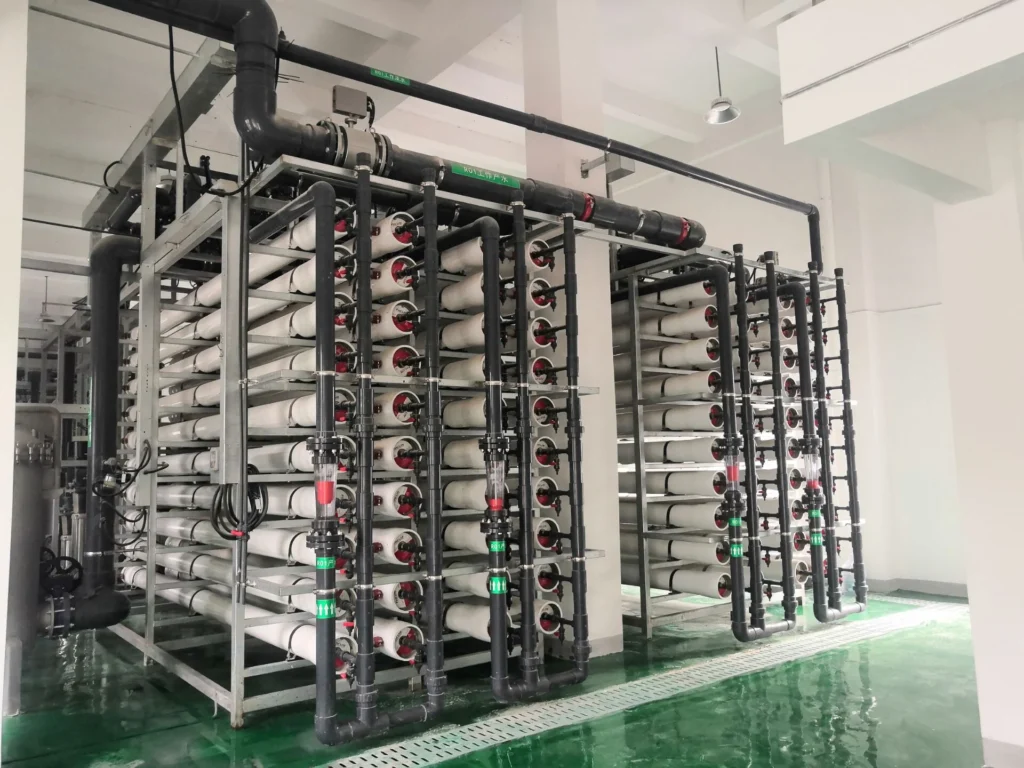
360 m³/h Chemical Plant Reclaimed-Water Reuse Retrofit
This 360 m³/h retrofit upgrades a chemical plant wastewater system for reclaimed-water reuse. Filtration, ultrafiltration, two-stage reverse osmosis and mixed-bed polishing are combined to supply the production-water system.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →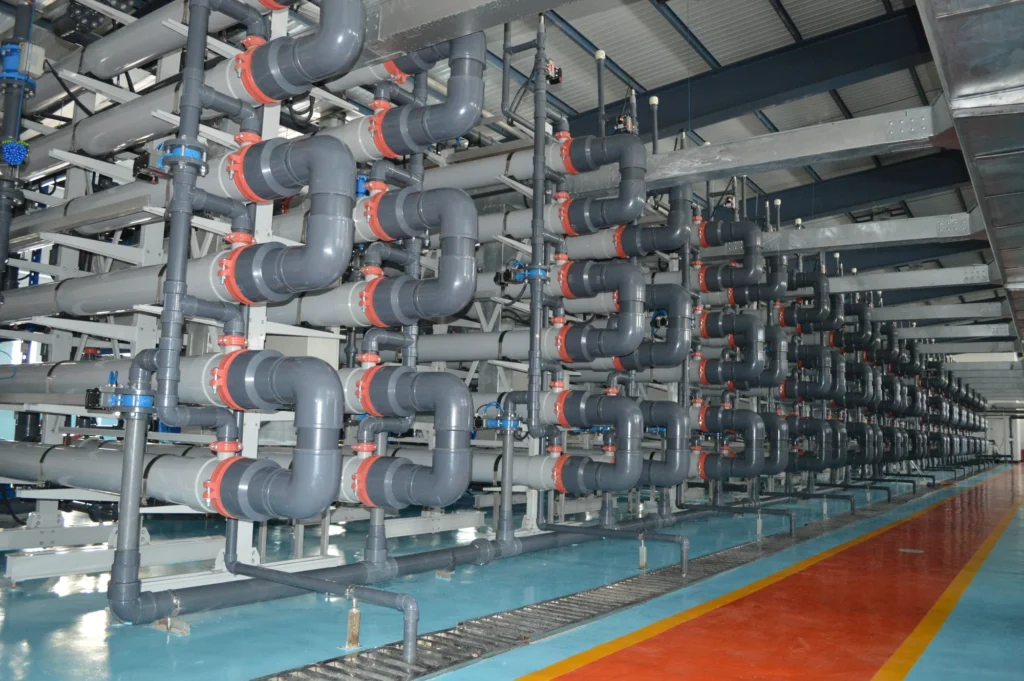
Industrial Wastewater Reuse & ZLD
10,000 m³/d Oilfield Produced-Water Deep Treatment Project
This 10,000 m³/d project treats oilfield produced water after oil-water separation. Tubular ultrafiltration is combined with electrodialysis and nanofiltration for deep treatment and subsequent reinjection use.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →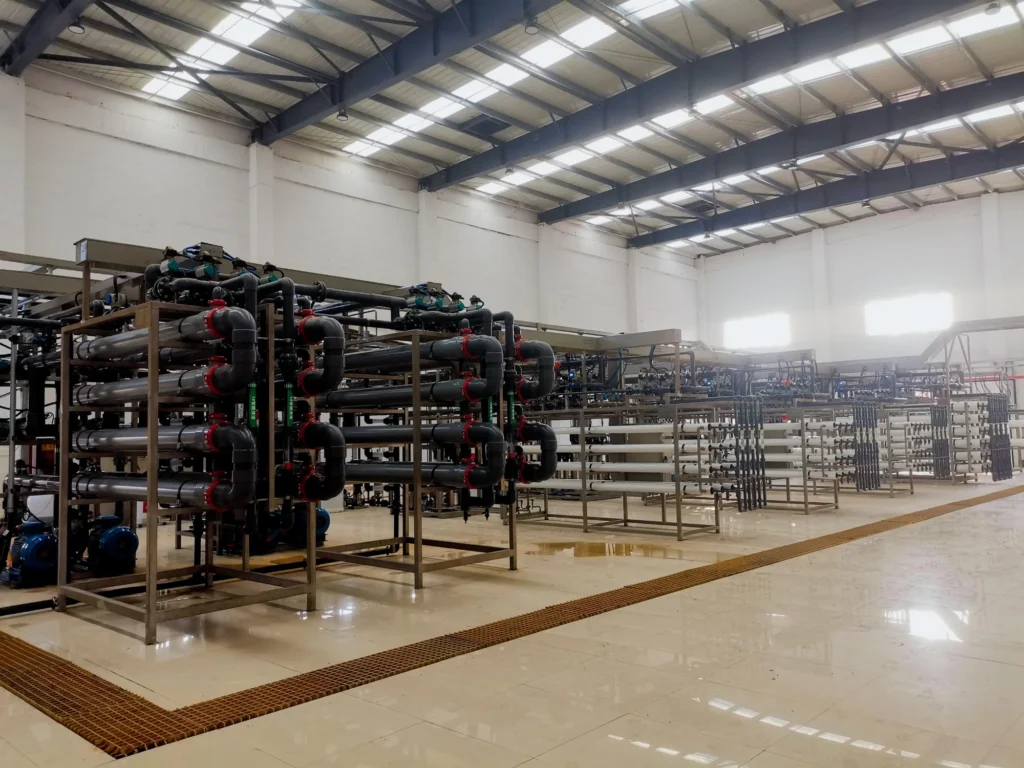
Industrial Wastewater Reuse & ZLD
1,200 m³/d Steel Pickling Wastewater Reuse and Resource Recovery Project
This project treats sulfuric-acid pickling wastewater from welding-wire production at a scale of 1,200 m³/d. It combines iron removal and softening, PEK tubular membranes, RO/NF, causticization, and evaporation and crystallization for water reuse and resource recovery.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →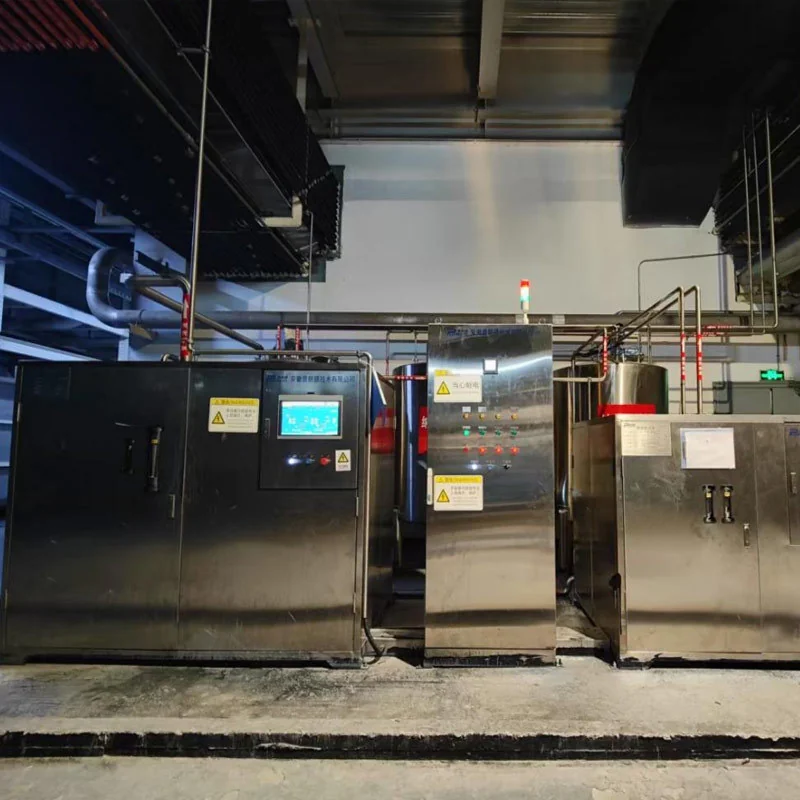
Industrial Wastewater Reuse & ZLD
0.4 m³/h Automotive Paint-Shop Cleaning-Liquid Recovery Project
This project treats water-based solvent cleaning waste liquid from an automotive paint shop at a scale of 0.4 m³/h. It combines ultrafiltration and nanofiltration for cleaning-liquid reuse and volume reduction.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →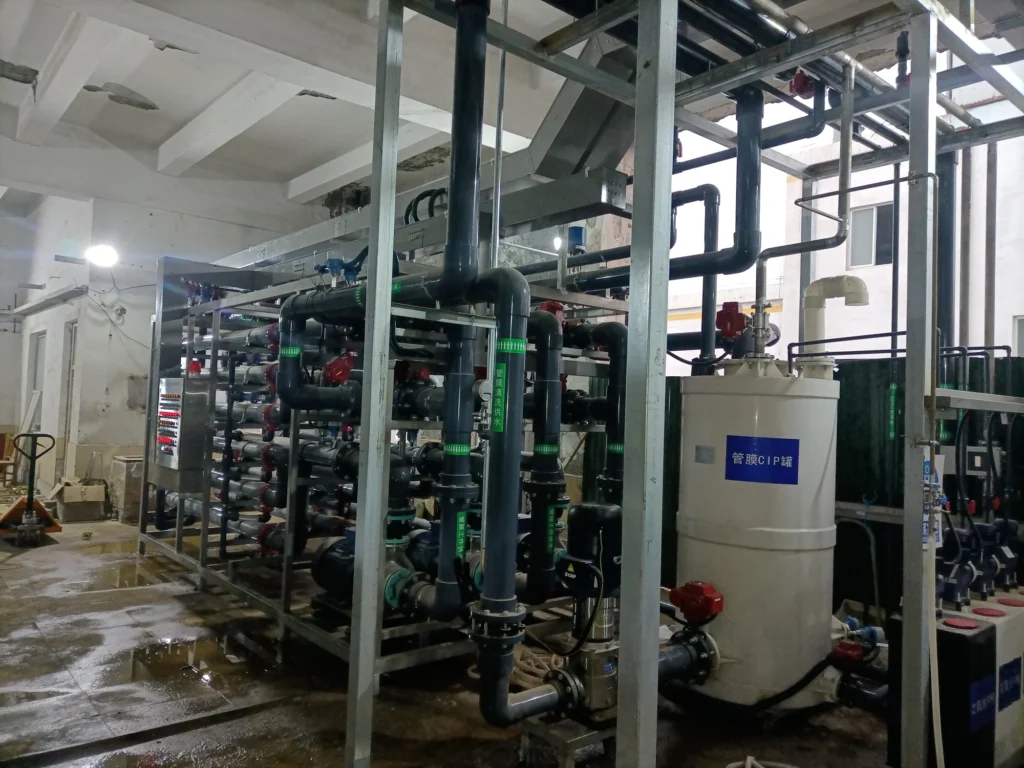
Industrial Wastewater Reuse & ZLD
2,400 m³/d High-Alkalinity Aluminum Production Wastewater Project
This project treats high-alkalinity wastewater from aluminum production at a scale of 2,400 m³/d. The process combines acidification, flocculation and settling pretreatment with PEK tubular membrane filtration and downstream reverse osmosis for water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →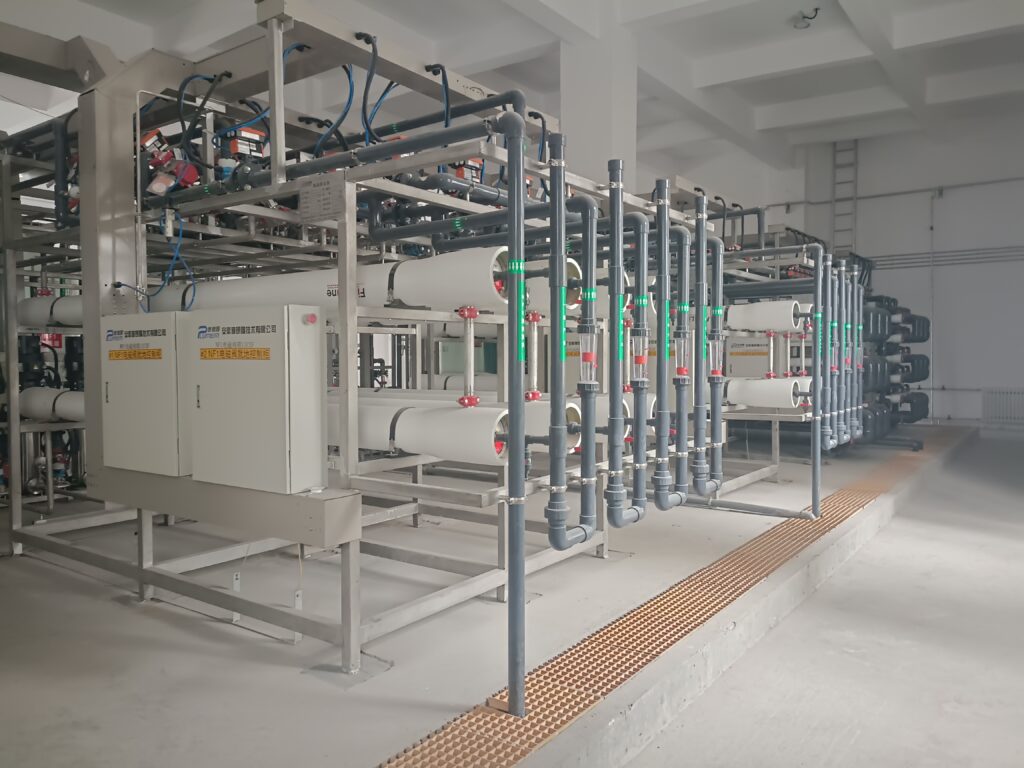
Industrial Wastewater Reuse & ZLD
10 m³/h FGD Wastewater ZLD Project
A 10 m³/h FGD wastewater ZLD project combining two-stage softening, PEK tubular membranes, NF salt separation and high-pressure RO. Plum supplied the process equipment except the evaporator.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →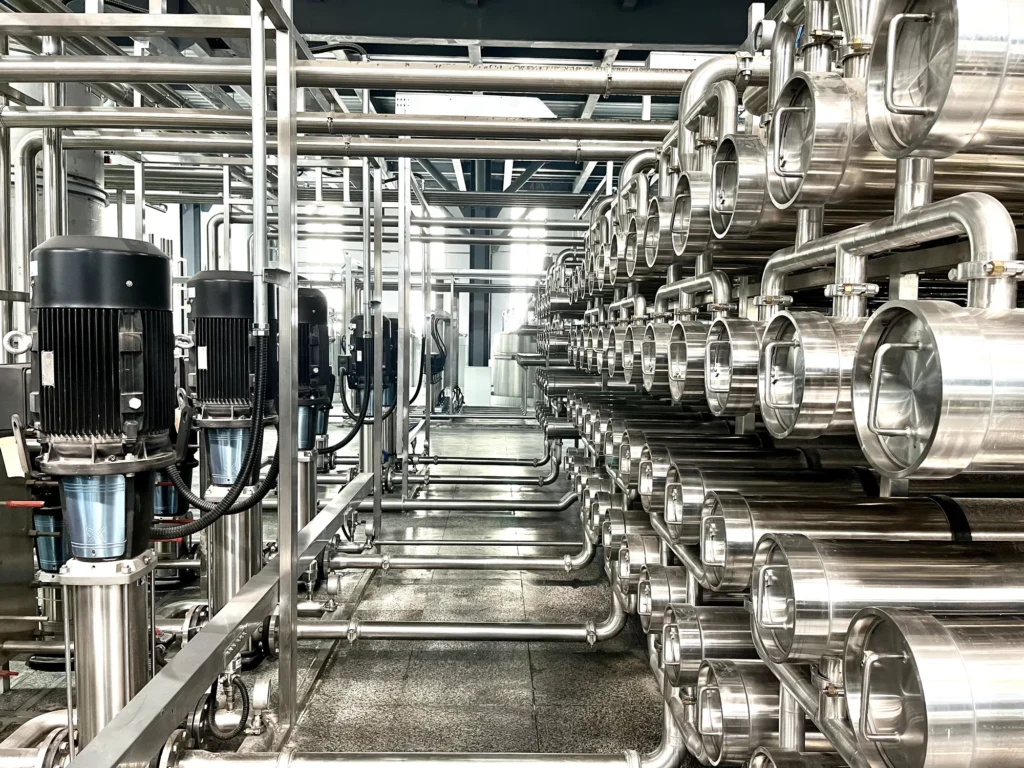
Process Fluid Membrane Separation
15 m³/h Lactic Acid Nanofiltration Purification
Separate color bodies, residual sugars, salts, and target product streams through a validated two-stage NF material balance.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →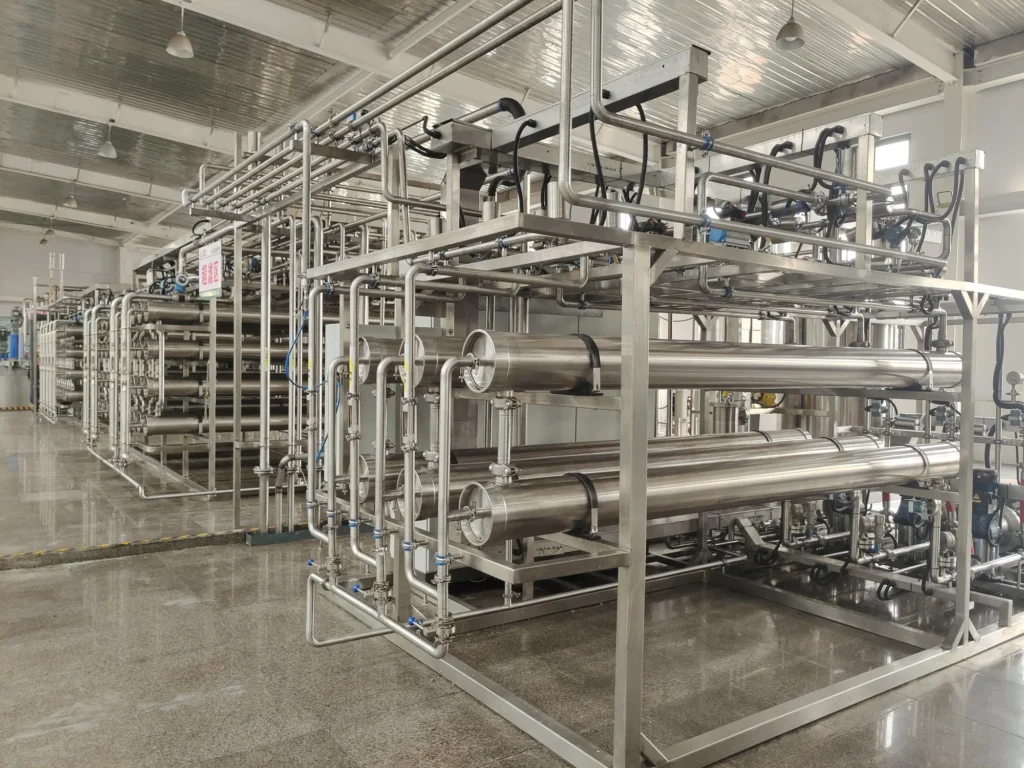
Process Fluid Membrane Separation
2,900 m³/d Allulose Membrane Purification
Connect clarification, fractionation, and concentration sections around the defined sugar profile and downstream product route.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →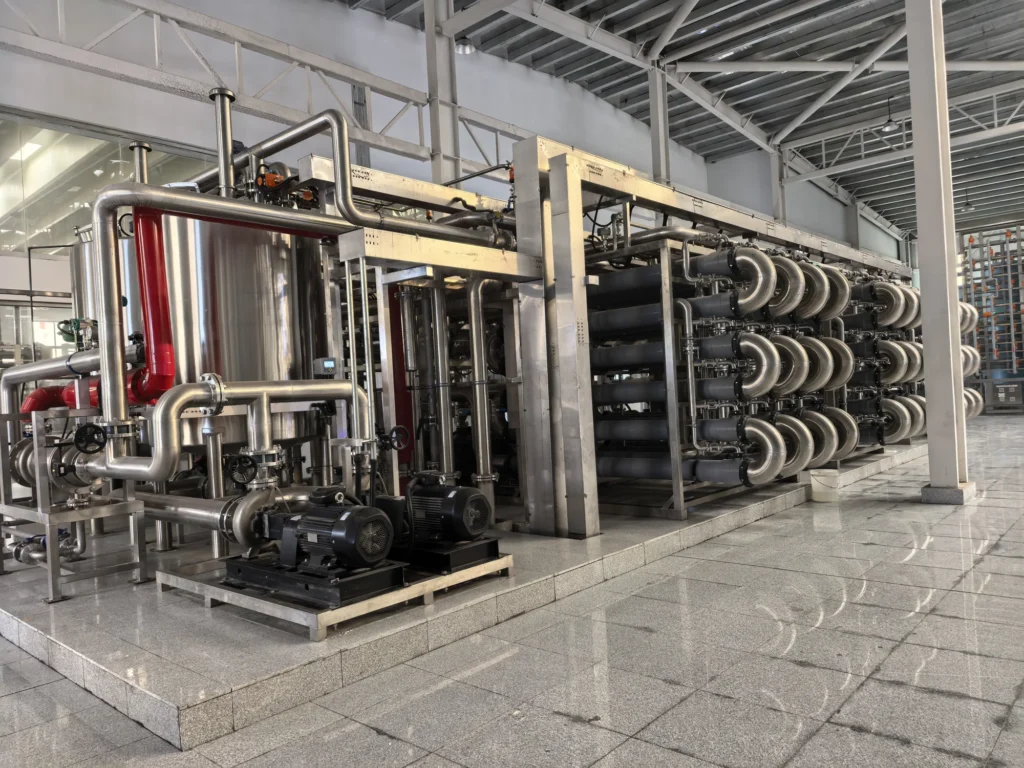
Process Fluid Membrane Separation
110 m³/h Starch Sugar Clarification
Remove suspended and colloidal material before project-defined refining and concentration operations.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →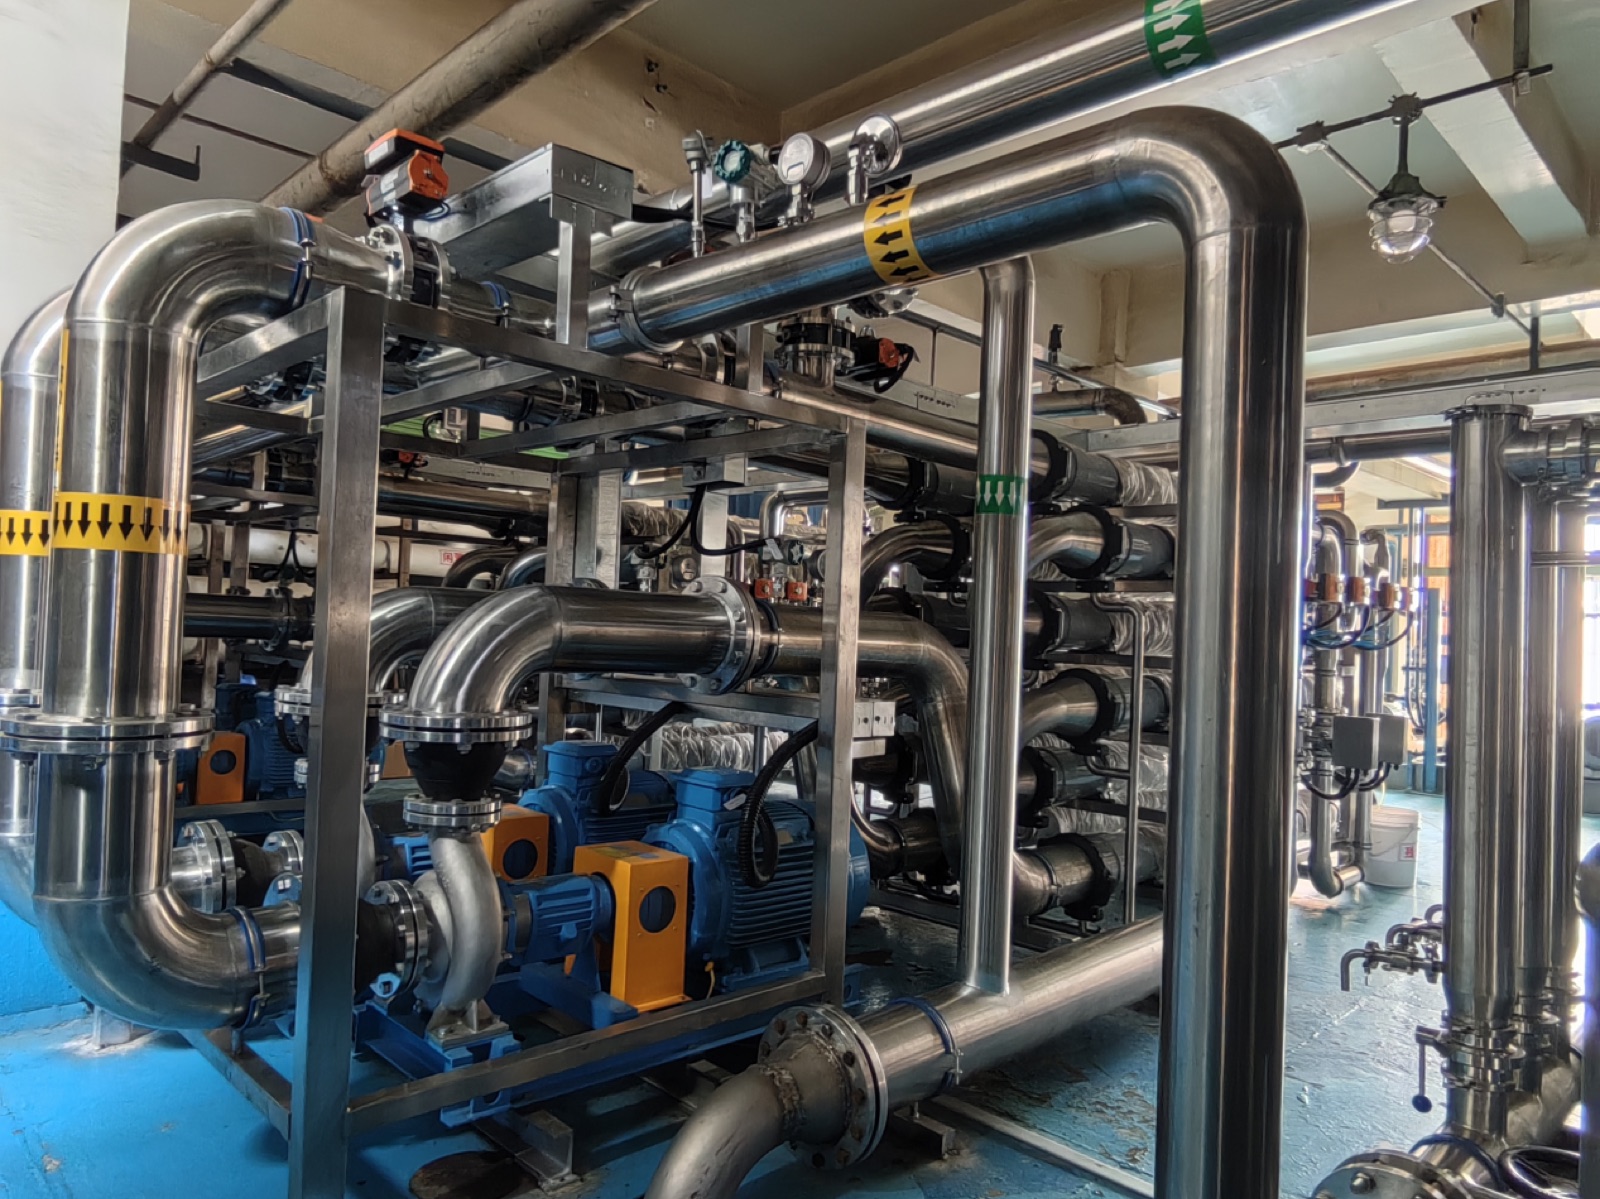
Process Fluid Membrane Separation
40 m³/h Fermentation Broth Clarification
Separate cells, solids, and suitable macromolecular impurities while defining both clarified and concentrated stream destinations.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →
Process Fluid Membrane Separation
50 m³/h Tea Extract Membrane Filtration
Clarify an aqueous botanical extract with PEK tubular UF, then concentrate the clarified extract with high-pressure RO before the spray-drying interface.
The capacity and membrane sections document this reference only; they do not establish design or performance for a new duty.
View case details →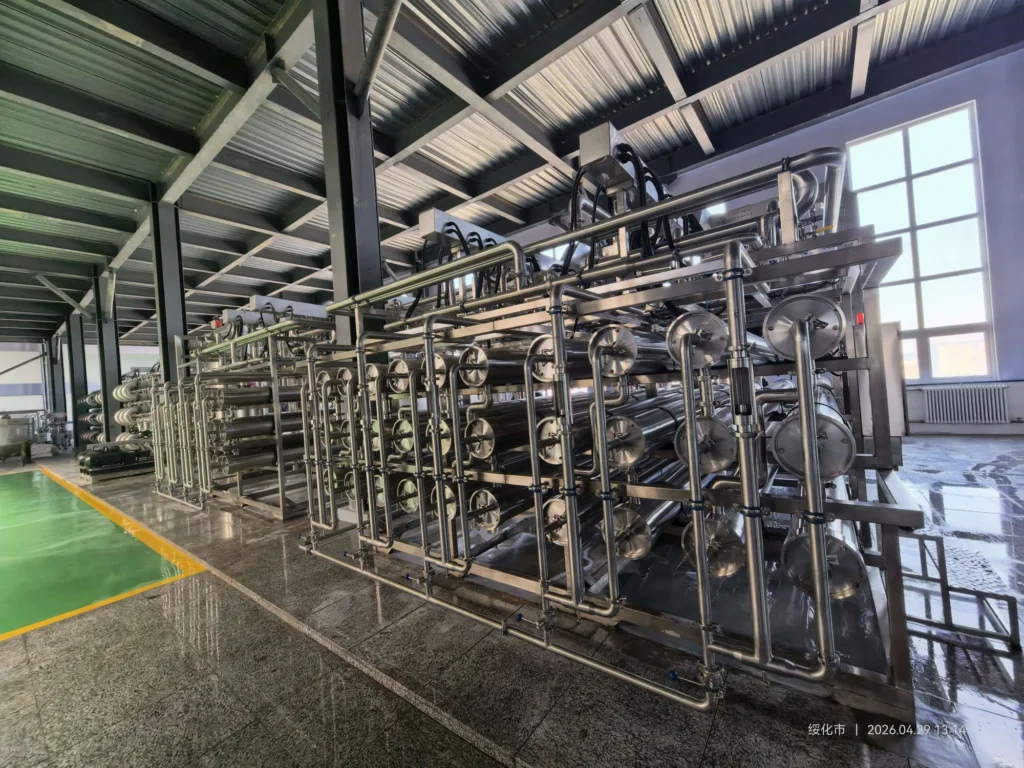
Process Fluid Membrane Separation
1,680 m³/d Tubular Membrane Clarification of Saccharified Liquor
This 1,680 m³/d project processes saccharified liquor. The membrane system continuously separates proteins, colloids, dextrins and other impurities. It replaces the former plate-and-frame filtration step and supplies clarified liquor for further refining.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →PROJECT CONTEXT