PROJECT EVIDENCE
Engineering Case Studies
Compare project scale, feed or process stream, and the membrane sections actually used across tubular membrane engineering, industrial wastewater reuse and ZLD, and process-fluid separation.
Showing 13–23 of 23
02 · INDUSTRIAL WATER
Industrial Wastewater Reuse & ZLD
References documenting reuse, brine, concentration, and leachate membrane sections with explicit project boundaries.
Industrial Wastewater Reuse & ZLD
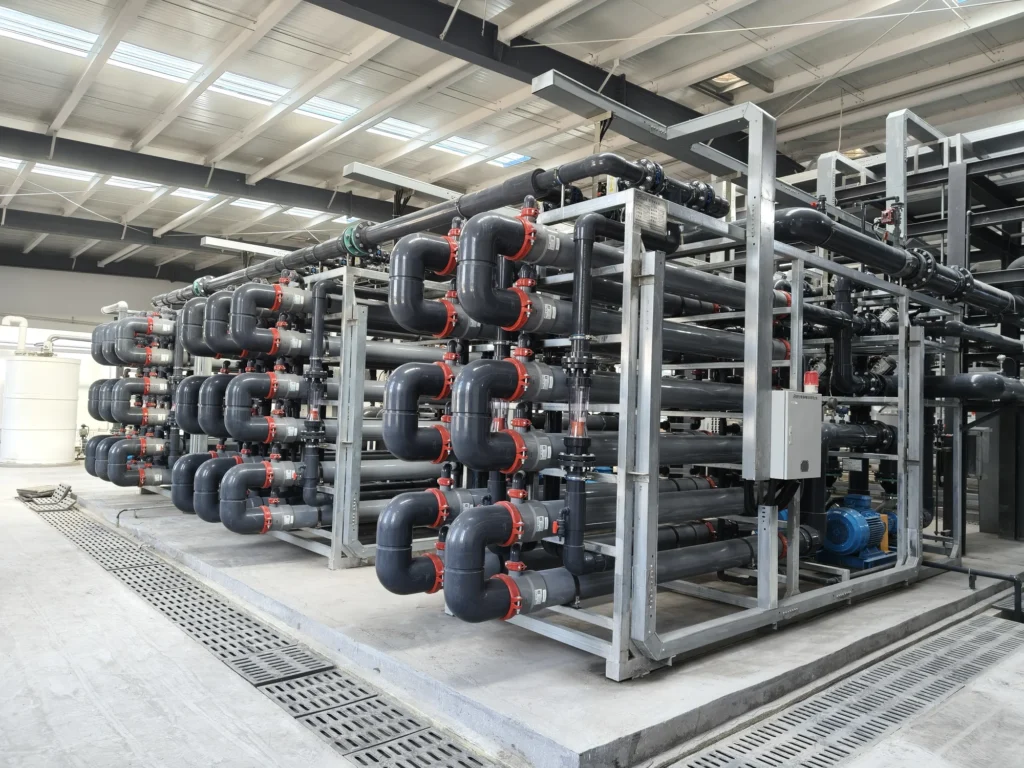
4,500 m³/d High-Salinity Mine-Water Reuse Project
This 4,500 m³/d project treats high-salinity, high-hardness mine water. Dual-alkali softening, alkali-resistant tubular ultrafiltration and reverse-osmosis concentration are combined for reuse in mine production and auxiliary water systems.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →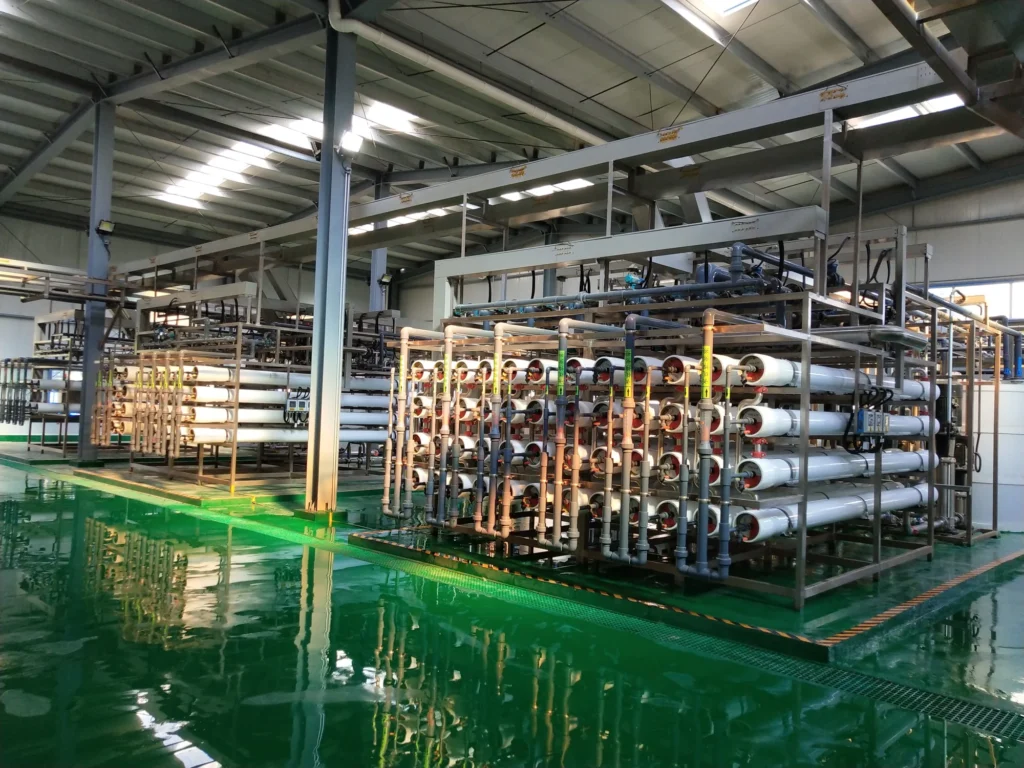
Industrial Wastewater Reuse & ZLD
3,200 m³/d Leachate and 640 m³/d Concentrate NF Treatment Project
This project has separate duties of 3,200 m³/d for landfill leachate and 640 m³/d for concentrate. Nanofiltration splitting and multistage concentrate treatment organize the permeate and concentrate streams for subsequent handling.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →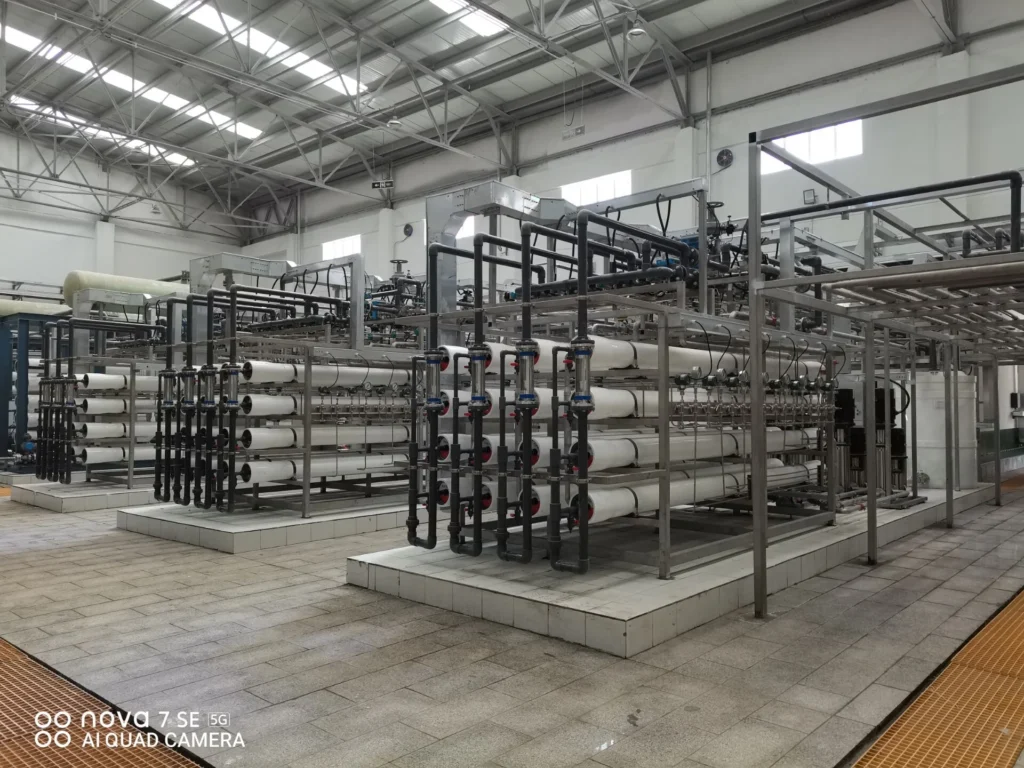
Industrial Wastewater Reuse & ZLD
25 m³/h Coal-Chemical Brine Salt-Separation Phase II Project
This phase II project treats 25 m³/h of coal-chemical RO brine. Ultrafiltration, nanofiltration salt separation, evaporation and crystallization are combined to process the resulting salt fractions.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →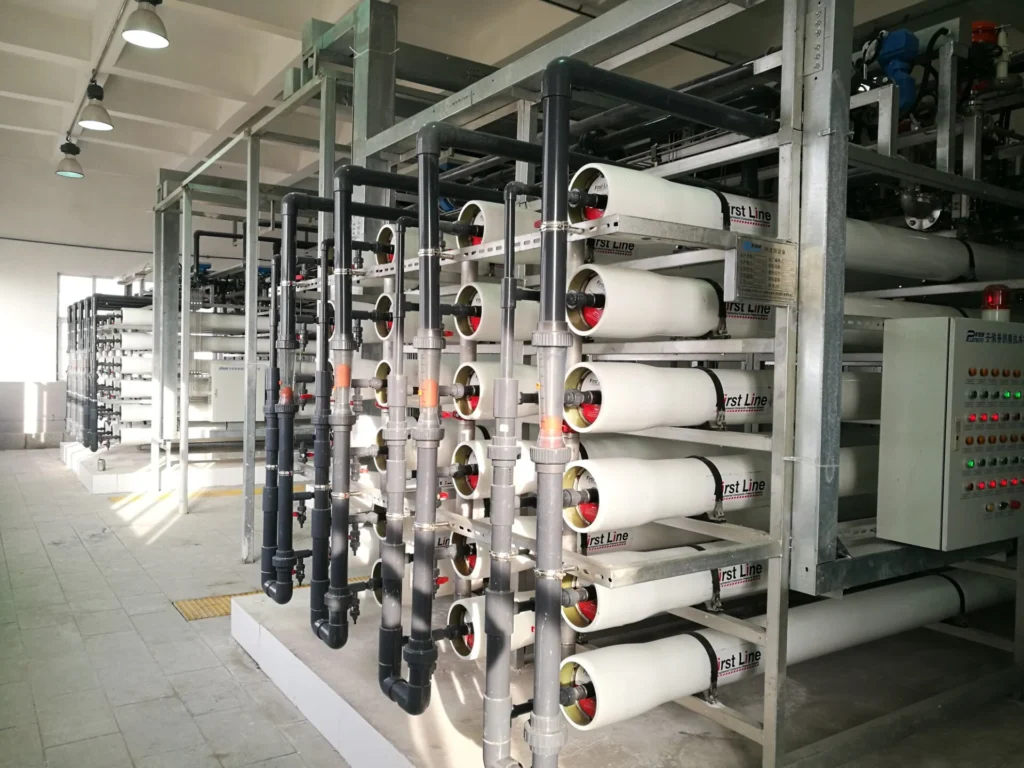
Industrial Wastewater Reuse & ZLD
60 m³/h RO Brine and 4 m³/h Mother-Liquor Salt-Separation Project
This coal-chemical project treats 60 m³/h of RO brine and 4 m³/h of crystallization mother liquor. The process combines ultrafiltration, two-stage nanofiltration, evaporation and crystallization, with a dedicated mother-liquor recovery duty.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →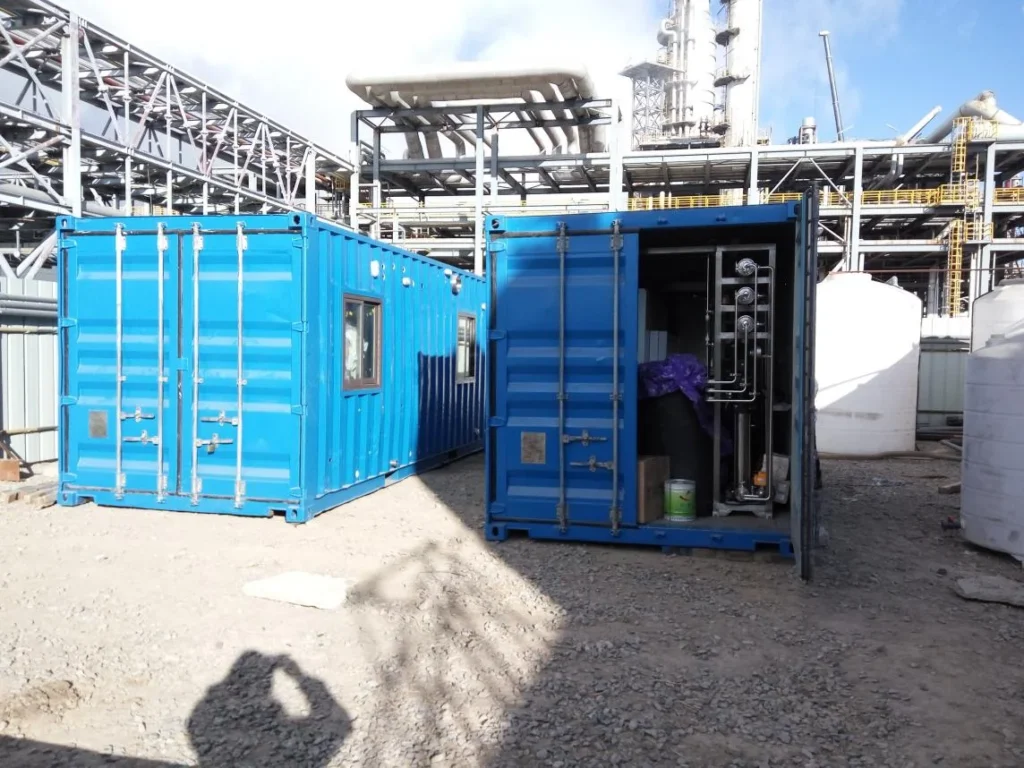
Industrial Wastewater Reuse & ZLD
24 m³/d RO Brine Reuse and Salt-Separation Pilot
This 24 m³/d pilot treats RO brine from coal-chemical production. Ultrafiltration and two-stage nanofiltration are combined to evaluate water reuse and selective salt treatment.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →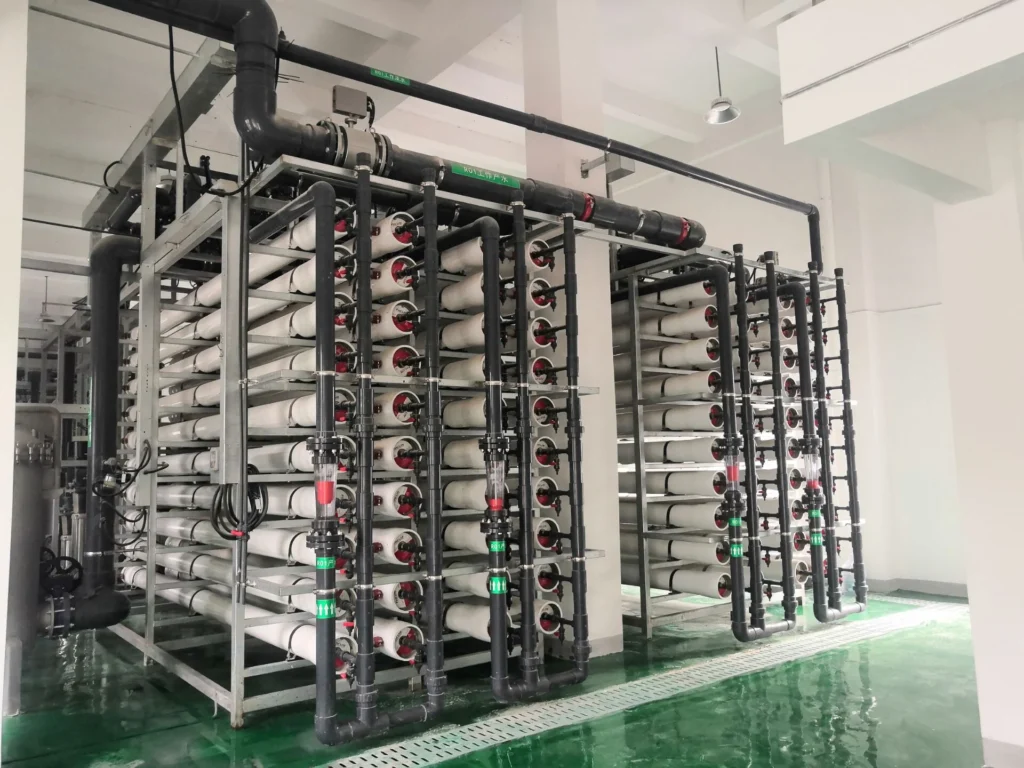
Industrial Wastewater Reuse & ZLD
360 m³/h Chemical Plant Reclaimed-Water Reuse Retrofit
This 360 m³/h retrofit upgrades a chemical plant wastewater system for reclaimed-water reuse. Filtration, ultrafiltration, two-stage reverse osmosis and mixed-bed polishing are combined to supply the production-water system.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →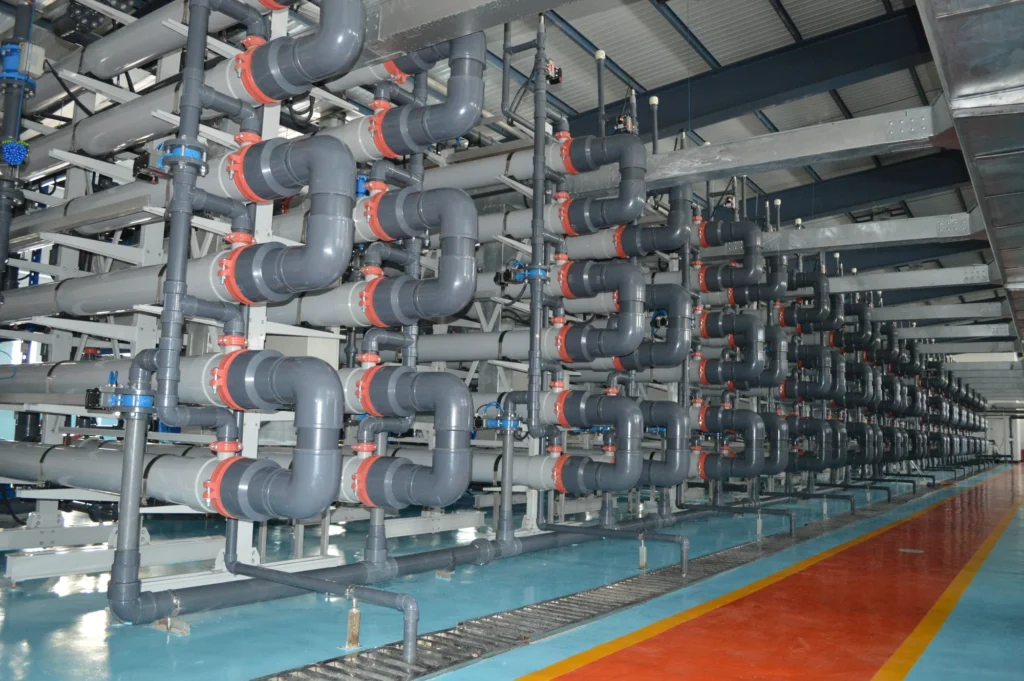
Industrial Wastewater Reuse & ZLD
10,000 m³/d Oilfield Produced-Water Deep Treatment Project
This 10,000 m³/d project treats oilfield produced water after oil-water separation. Tubular ultrafiltration is combined with electrodialysis and nanofiltration for deep treatment and subsequent reinjection use.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →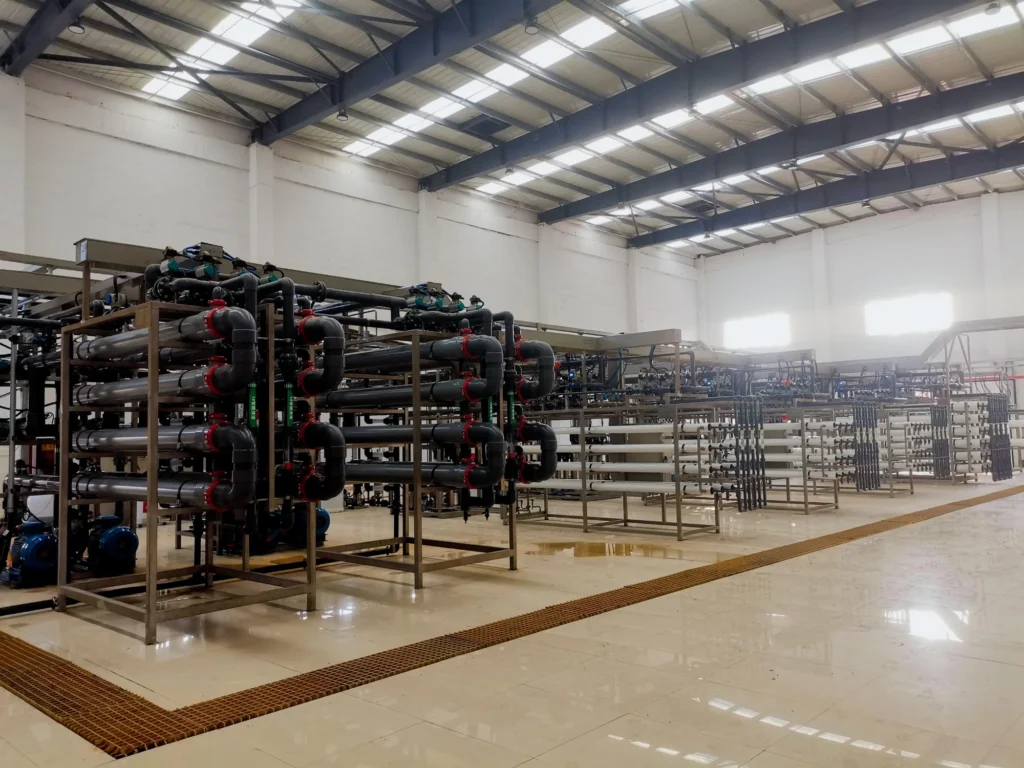
Industrial Wastewater Reuse & ZLD
1,200 m³/d Steel Pickling Wastewater Reuse and Resource Recovery Project
This project treats sulfuric-acid pickling wastewater from welding-wire production at a scale of 1,200 m³/d. It combines iron removal and softening, PEK tubular membranes, RO/NF, causticization, and evaporation and crystallization for water reuse and resource recovery.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →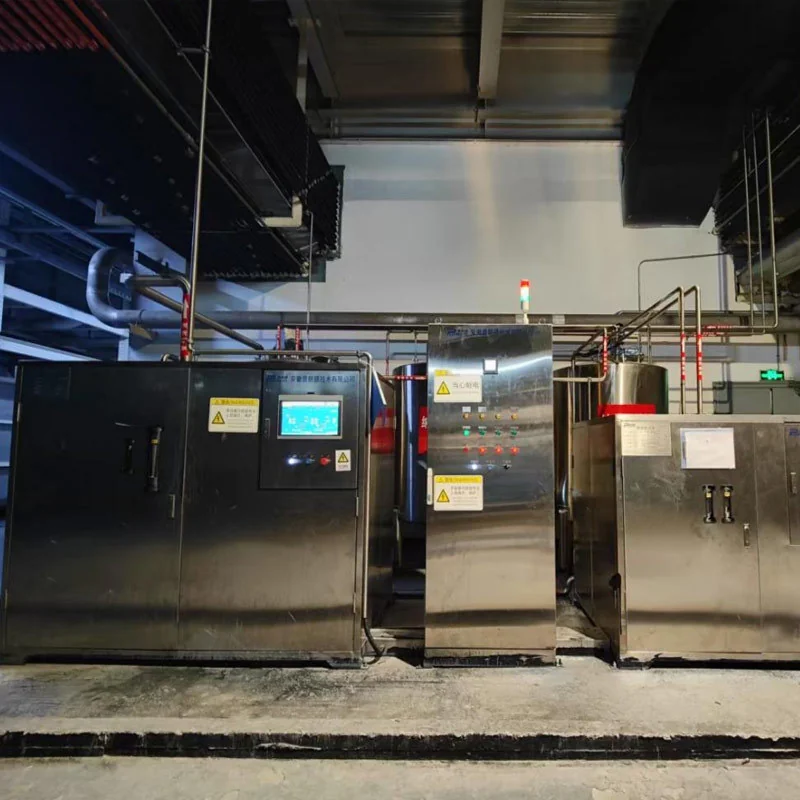
Industrial Wastewater Reuse & ZLD
0.4 m³/h Automotive Paint-Shop Cleaning-Liquid Recovery Project
This project treats water-based solvent cleaning waste liquid from an automotive paint shop at a scale of 0.4 m³/h. It combines ultrafiltration and nanofiltration for cleaning-liquid reuse and volume reduction.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →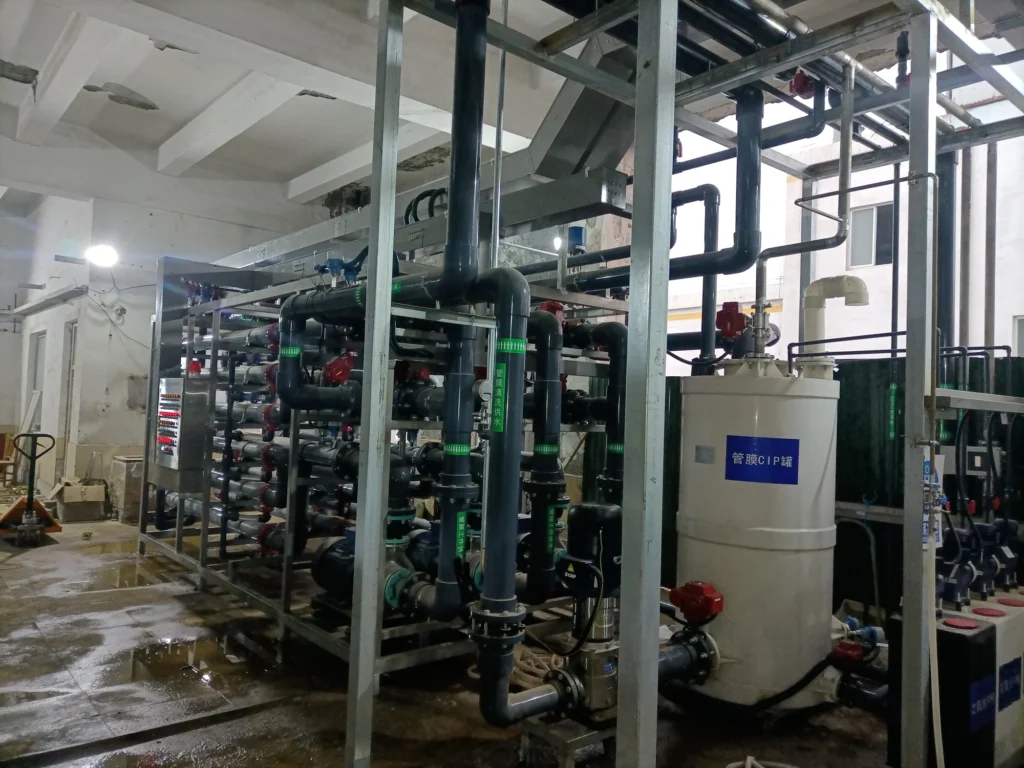
Industrial Wastewater Reuse & ZLD
2,400 m³/d High-Alkalinity Aluminum Production Wastewater Project
This project treats high-alkalinity wastewater from aluminum production at a scale of 2,400 m³/d. The process combines acidification, flocculation and settling pretreatment with PEK tubular membrane filtration and downstream reverse osmosis for water reuse.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →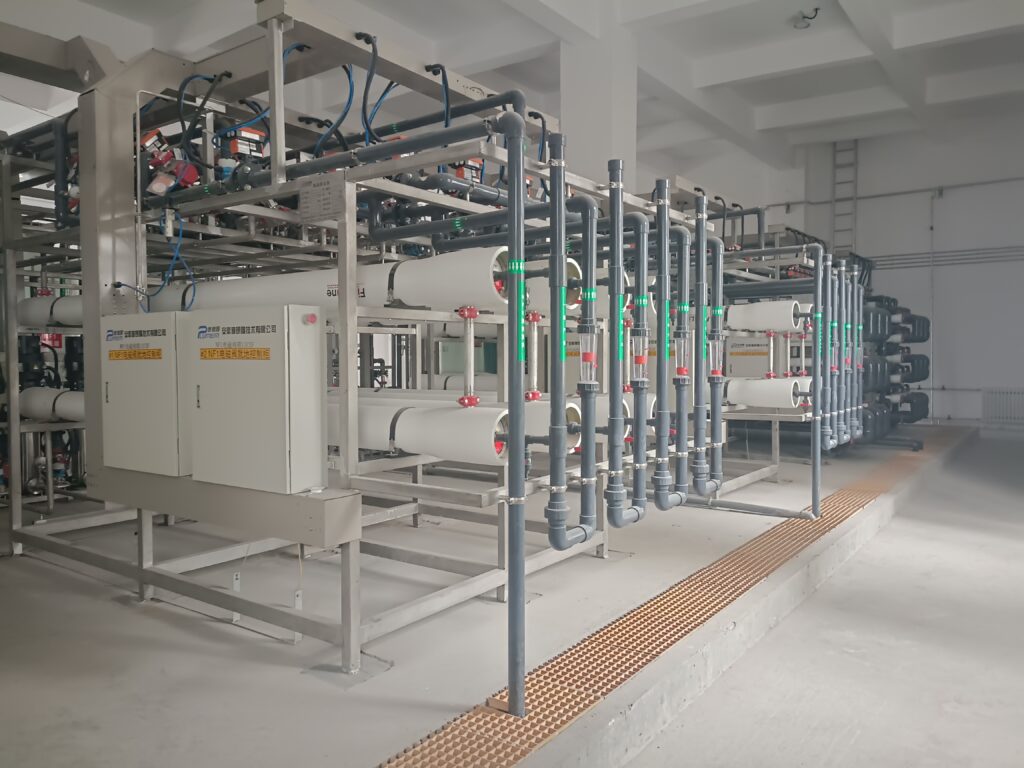
Industrial Wastewater Reuse & ZLD
10 m³/h FGD Wastewater ZLD Project
A 10 m³/h FGD wastewater ZLD project combining two-stage softening, PEK tubular membranes, NF salt separation and high-pressure RO. Plum supplied the process equipment except the evaporator.
This reference is for comparison; a new duty requires its own engineering validation.
View case details →PROJECT CONTEXT