Case study
40 m³/h Lactic Acid Condensate Recovery and Concentration
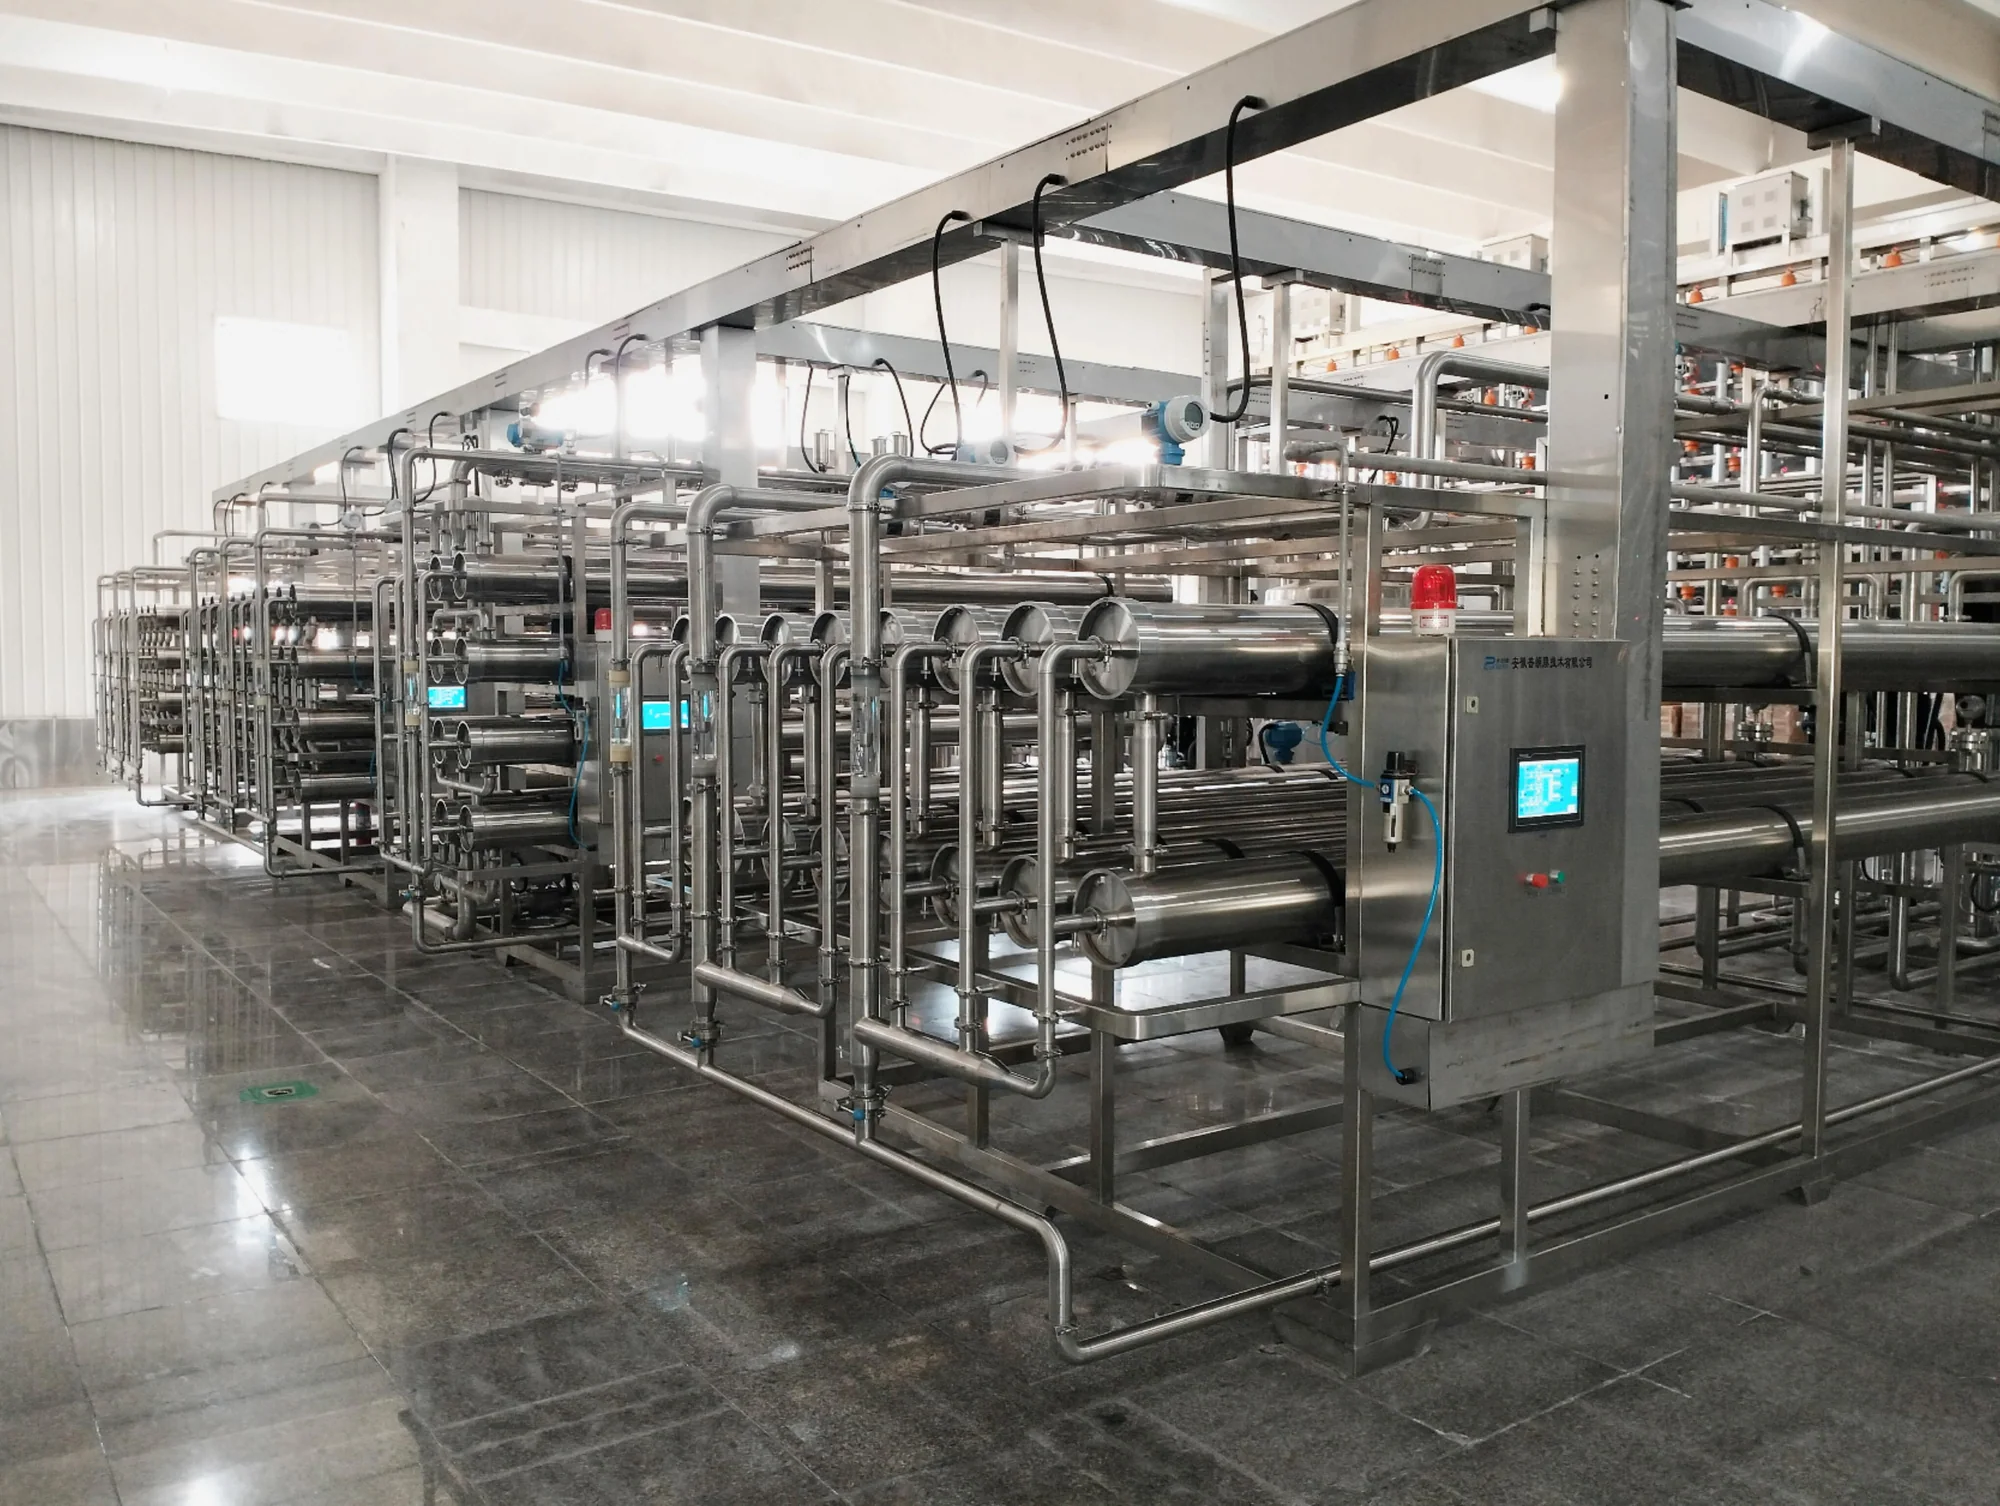
This 40 m³/h project processes dilute lactic acid liquor in evaporation condensate. The membrane stage recovers dilute lactic acid from evaporation condensate. Permeate returns to process-water reuse and concentrate proceeds to evaporation. This case and the 20 m³/h lactic-acid NF case cover different sections at the same plant.
Project overview
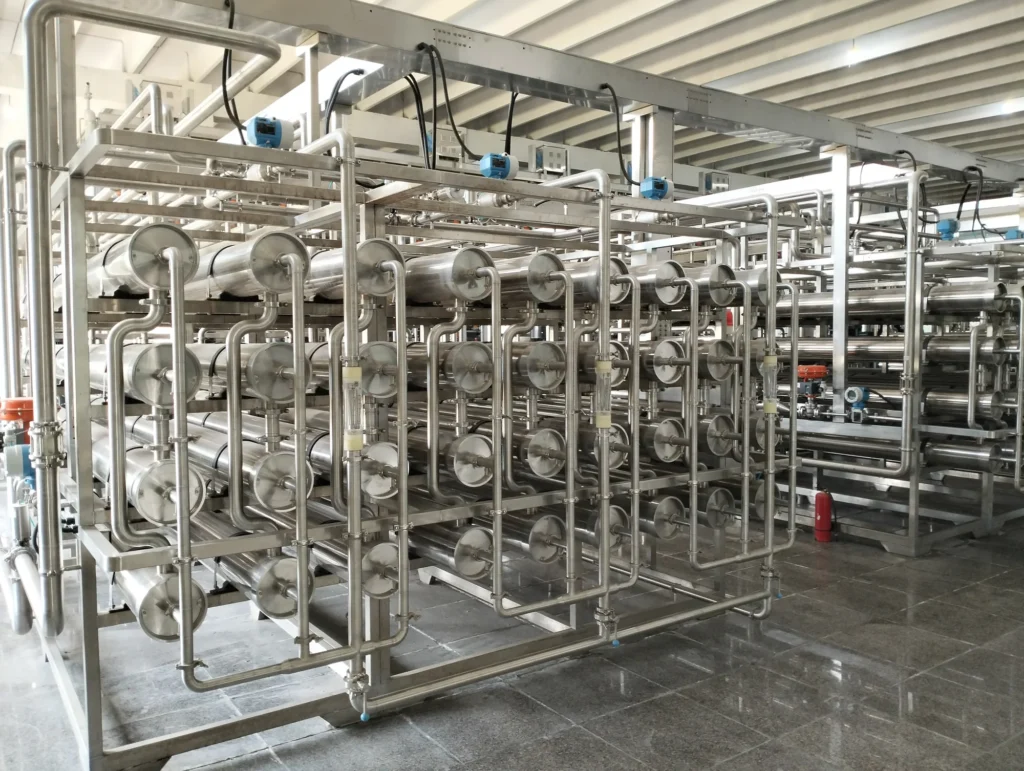
This 40 m³/h project processes dilute lactic acid liquor in evaporation condensate.
Membrane process
High-pressure membrane recovery and concentration + permeate reuse + evaporation interface
Process roles
The membrane stage recovers dilute lactic acid from evaporation condensate. Permeate returns to process-water reuse and concentrate proceeds to evaporation. This case and the 20 m³/h lactic-acid NF case cover different sections at the same plant.
Project photos